
Metal Injection Molding and investment casting can both produce complex metal components, but they solve different manufacturing problems. MIM is usually the stronger candidate when a part is small, geometrically detailed, difficult to machine, and required in repeatable medium-to-high production volume. Investment casting remains practical when the component is larger, the volume is lower to medium, the alloy route is better established for casting, or critical features can be machined after casting without losing the project’s cost advantage.
Quick answer: choose Metal Injection Molding when the part is small, complex, high-volume, and benefits from molded fine features that reduce machining or assembly. Choose investment casting when the part is larger, lower-to-medium volume, better suited to a cast alloy route, or still requires post-casting machining on critical surfaces. The correct decision depends on drawing geometry, section thickness, material route, tolerance zones, annual volume, surface requirements, quality risks, and the cost of the accepted finished part.
For an actual part, process selection should be based on whether the production route remains stable after tooling, material selection, dimensional control, surface finishing, inspection, yield, and total cost are considered. This is especially important when deciding whether an existing investment-cast part should remain cast or be redesigned for MIM.
Quick Selection Table: When to Choose MIM or Investment Casting
| Project Factor | Choose MIM When... | Choose Investment Casting When... |
|---|---|---|
| Part size | The part is small, compact, or palm-sized, and the powder cost does not dominate the project. | The part is medium to large, heavy, or too bulky for economical debinding and sintering. |
| Geometry | The design has small holes, grooves, undercuts, thin walls, fine details, or multiple features that would be expensive to machine. | The geometry is complex but better suited to wax pattern creation, shell molding, casting flow, and post-casting finishing. |
| Production volume | Annual volume is medium to high and tooling can be amortized across repeat production. | Volume is low to medium and the project needs casting flexibility more than multi-cavity production efficiency. |
| Material route | The alloy is available as a proven MIM feedstock and has a stable sintering route. | The alloy is better established as a cast alloy or is specified by the customer as a casting route. |
| Tolerance | Repeatable small-part dimensional control is important and critical features can be supported through MIM tooling and sintering strategy. | Critical features can be machined after casting without making the total finished part cost unattractive. |
| Surface finish | Fine feature detail and reduced secondary machining are valuable. | Cast surface plus grinding, blasting, polishing, or machining is acceptable. |
| Cost driver | Finished part cost improves by reducing machining, assembly, scrap, or inspection sorting over volume. | Lower initial tooling cost or larger-part casting economics matter more. |
| Best fit | Small complex precision metal parts. | Larger complex cast metal parts. |
Treat this table as an initial screening tool rather than a tooling decision. Before tooling, review the drawing, material grade, critical tolerances, section thickness, annual volume, inspection method, and operating conditions.
Why Investment Casting and Die Casting Need Separate Comparisons
Investment casting and die casting are both casting routes, but they create different engineering and cost tradeoffs. Investment casting uses a lost-wax route with wax patterns, ceramic shells, dewaxing, molten metal pouring, shell removal, and finishing. Die casting uses high-pressure injection of molten metal into a steel die, typically for high-volume non-ferrous parts.
If the competing process is high-pressure die casting rather than lost-wax investment casting, review MIM vs die casting. That decision depends more heavily on pressure-casting alloy limits, draft and flash, porosity, die tooling cost, and high-volume cycle economics. Investment-casting projects require a different review centered on cast-part geometry, alloy route, post-casting machining, and whether redesign for MIM creates enough manufacturing value.
What Is the Main Difference Between MIM and Investment Casting?
MIM Uses Feedstock Injection, Debinding, and Sintering
Metal Injection Molding starts with fine metal powder mixed with a binder system to form moldable feedstock. This MIM feedstock is injected into a precision mold to form a green part. The binder is then removed through the MIM debinding process, and the remaining brown part is sintered to densify the metal structure and reach the final geometry.
MIM is not a molten-metal casting process. The part is shaped in a mold, but the final metal component is created through powder metallurgy and MIM sintering. The tool must compensate for sintering shrinkage, and the part design must allow stable binder removal, controlled support, and repeatable dimensional change.
Investment Casting Uses Wax Patterns, Ceramic Shells, and Molten Metal Pouring
Investment casting, also called lost wax casting, follows a different manufacturing route. A wax pattern is produced, assembled onto a wax tree, coated with ceramic slurry and stucco to form a ceramic shell, then dewaxed before molten metal is poured into the shell cavity. After solidification, the shell is removed and finishing operations are applied where needed.
Investment-casting quality depends on wax pattern accuracy, shell building, gating, metal flow, solidification, shrinkage, shell removal, and post-casting finishing. These control points differ from MIM, even when both processes are being considered for a near-net-shape metal component.
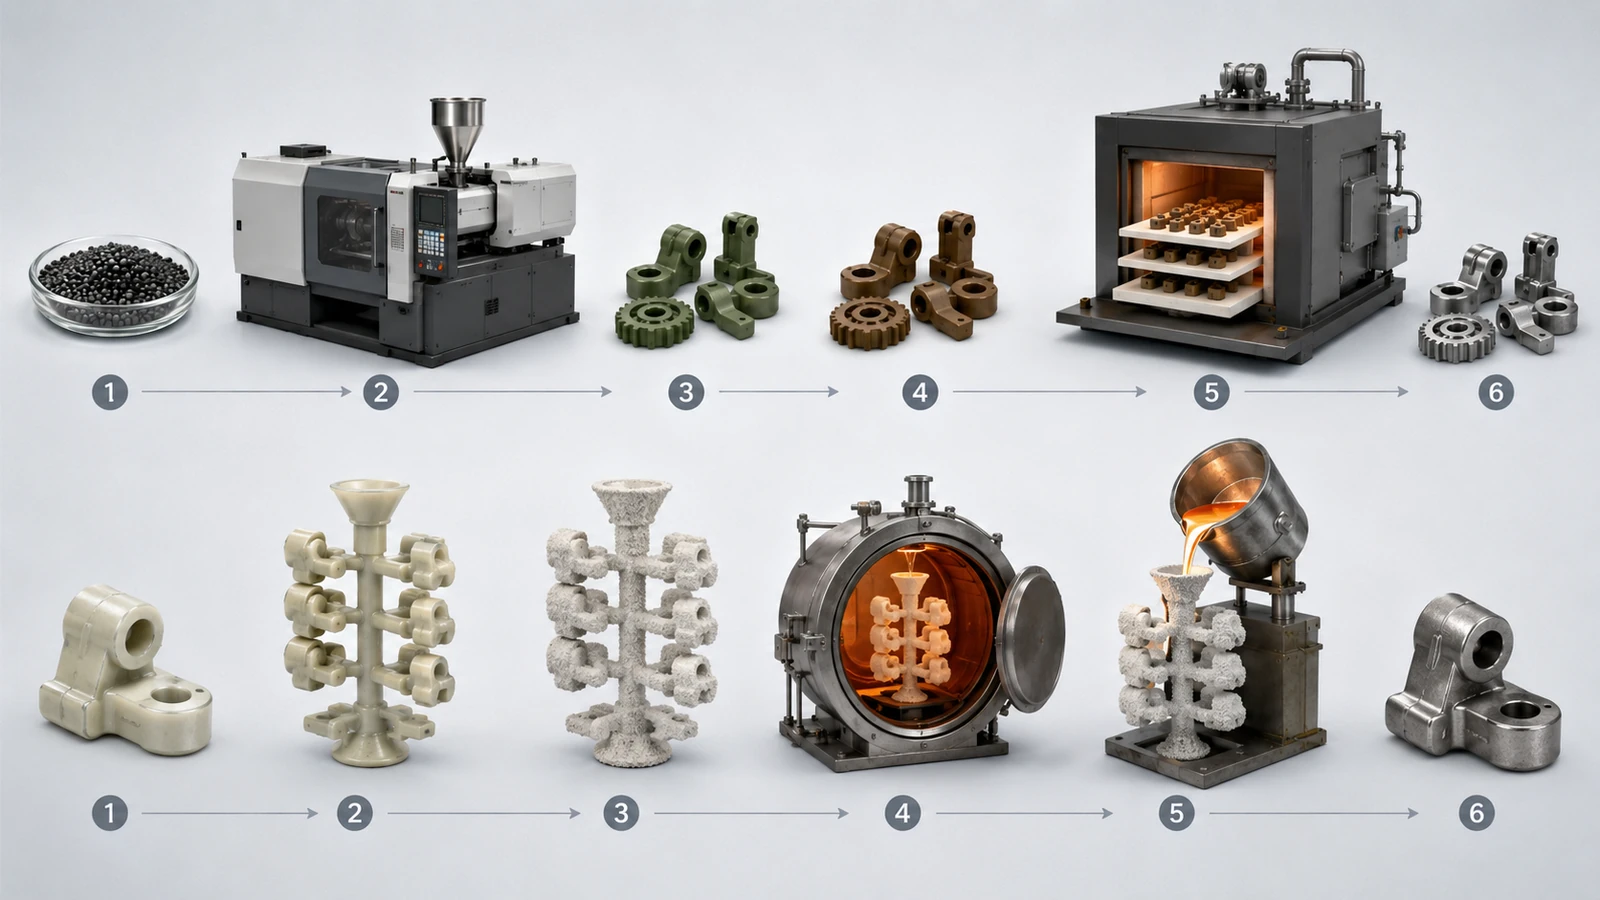
MIM vs Investment Casting: Process Comparison Table
| Comparison Point | Metal Injection Molding | Investment Casting |
|---|---|---|
| Forming principle | Injected metal powder feedstock | Wax pattern and ceramic shell casting |
| Material state during forming | Fine metal powder + binder feedstock | Molten metal poured into a ceramic shell |
| Tooling logic | Injection mold with shrinkage compensation and gate/parting line strategy | Wax tooling, tree assembly, ceramic shell building, gating, and riser/feed design |
| Key thermal stage | Debinding and sintering | Dewaxing, shell preheating, pouring, and solidification |
| Shrinkage mechanism | Controlled sintering shrinkage | Solidification and cooling shrinkage |
| Typical strength | Small complex near-net-shape metal components | Larger or broader cast metal components |
| Key process risk | Short shot, debinding cracks, sintering distortion, shrinkage variation, support marks | Porosity, shrinkage cavities, shell defects, inclusions, gate removal marks |
| Best decision use | High-volume small precision parts | Larger or lower-volume precision cast parts |
A common mistake is to compare only the near-net-shape claim of each process. Both processes can reduce machining compared with full CNC machining, but they achieve shape, density, surface, and dimensional control in different ways.
Part Size, Weight, and Section Thickness: Where Each Process Becomes Practical
Why MIM Is Usually Stronger for Small Complex Parts
MIM is most valuable when the part is small enough for stable molding, debinding, sintering, and batch handling, but complex enough that machining or casting plus finishing becomes inefficient. Good candidates often include small brackets, hinges, medical device parts, lock components, electronic hardware, miniature structural parts, and precision mechanisms.
The advantage is not only size. The stronger MIM case usually comes from the combination of compact size, complex geometry, repeatable production, and reduced secondary machining. If a part has multiple small holes, thin features, side grooves, fine details, or difficult-to-machine shapes, MIM may form these features directly from the mold.
Why Investment Casting Is Often Better for Larger Cast Components
Investment casting is often more practical for larger components, thicker sections, and lower-to-medium production volumes. If the part is too large, too heavy, or too thick for economical MIM, investment casting may provide a more practical route. It also remains valuable when the material is better suited to casting or when critical surfaces can be machined after casting.
For larger structural cast parts, the cost of MIM powder, tooling, debinding time, sintering control, and distortion risk may outweigh the benefit of injection-molded geometry.
Why Section Thickness Matters Before Choosing MIM
Section thickness is often more important than the overall envelope size. A small part with thick, uneven sections may still be difficult for MIM because binder removal and sintering shrinkage must remain stable. Thick regions can increase the risk of debinding defects, internal stress, distortion, or nonuniform shrinkage.
For investment casting, section thickness also matters, but for different reasons. The casting engineer must consider metal flow, feeding, hot spots, solidification, and shrinkage cavities. A design that works in investment casting is not automatically suitable for MIM without DFM review.
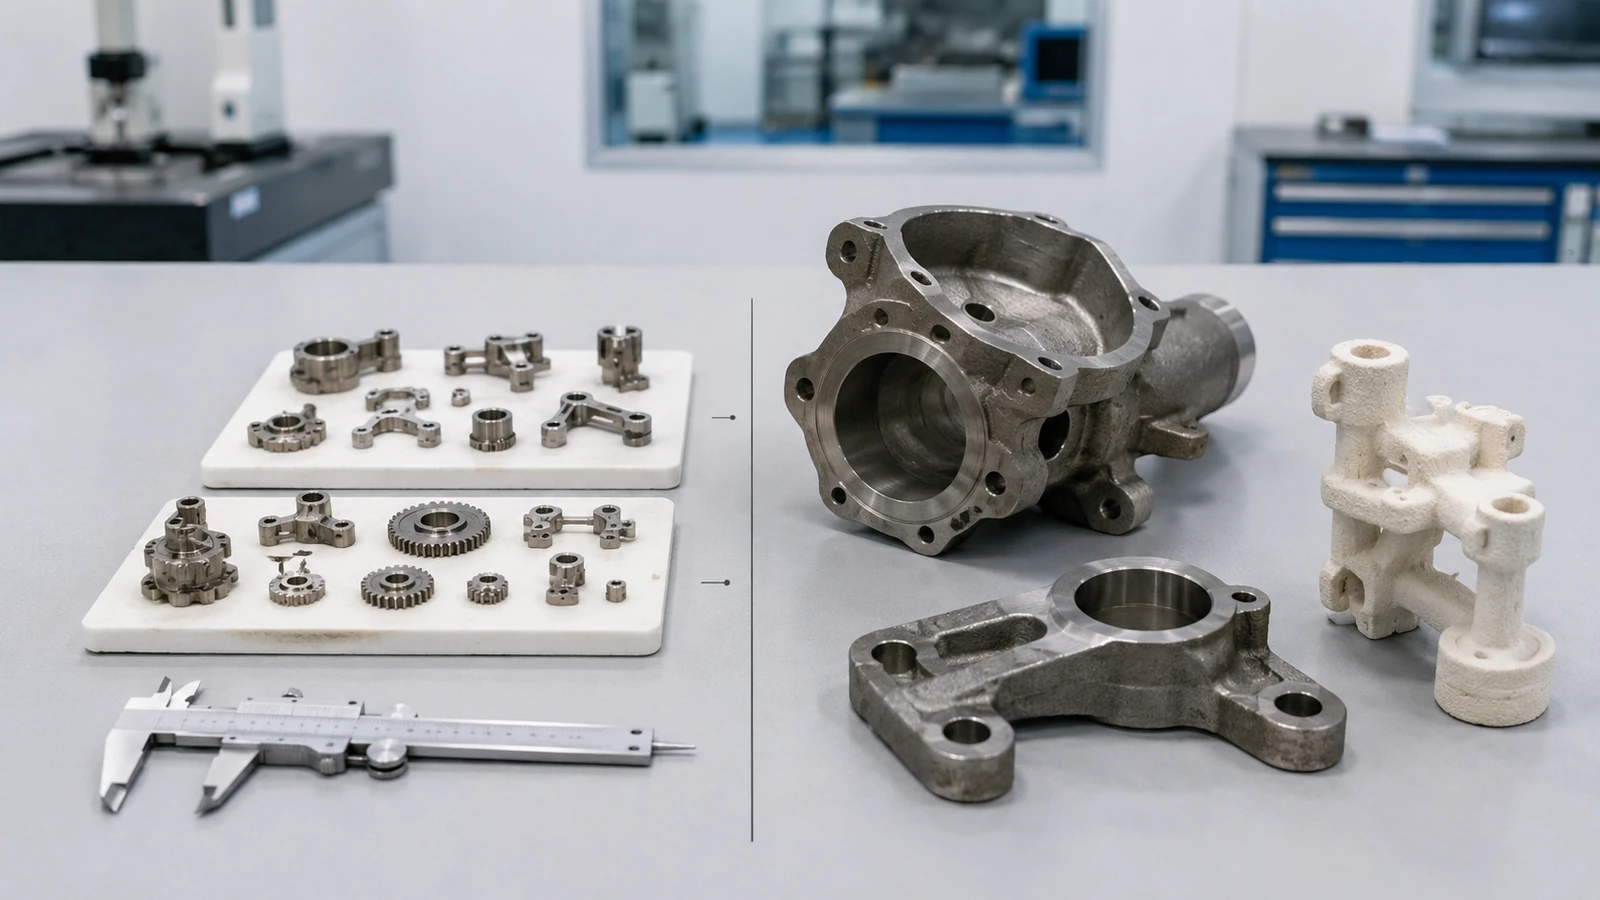
MIM Technical Red Flags to Check Before Tooling
A part that looks favorable for MIM in an initial comparison can still become difficult, unstable, or uneconomical if key DFM conditions are not resolved. The following items are screening flags to check before tooling, not universal production limits.
| Review Item | MIM Red Flag | What to Confirm Before Tooling |
|---|---|---|
| Part envelope | Large, heavy, or bulky geometry where powder cost, debinding time, furnace loading, and distortion risk may dominate. | Confirm part mass, furnace handling, sintering support, and whether the geometry still provides enough machining or assembly reduction to justify MIM. |
| Section thickness | Very thick, highly uneven sections or isolated mass concentrations connected to thin features. | Review binder-removal paths, thick-to-thin transitions, distortion risk, and whether non-functional material can be reduced or redistributed. |
| Annual volume | Low or uncertain repeat demand that cannot justify dedicated tooling and process validation. | Compare tooling amortization and finished-part cost against investment casting, CNC machining, or another lower-commitment route. |
| Feature value | Simple geometry where most functional features still need machining after sintering. | Identify which holes, grooves, slots, teeth, splines, undercut-like features, or consolidated functions can actually be molded and remove secondary operations. |
| Material route | The specified alloy lacks a practical MIM feedstock, stable sintering window, or verified property route. | Confirm powder and feedstock availability, sintering behavior, heat treatment, density, corrosion or mechanical requirements, and application-specific acceptance criteria. |
| Critical tolerances | Tight tolerances are applied across the drawing without clear datum priority or allowance for secondary operations. | Separate critical from non-critical dimensions and define which features rely on tooling compensation, sintering support, sizing, inspection control, or limited machining. |
EPMA MIM design guidance also treats tolerance, surface finish, part size, and section thickness as process-dependent factors that should be confirmed for the actual part and production route. See EPMA MIM design guidance.
Geometry and Design Complexity: Which Process Handles Fine Features Better?
Where MIM Has a Clear Advantage
MIM is usually stronger when a small metal part requires fine features that would be expensive to machine or difficult to hold consistently after casting. Typical MIM-friendly features may include:
- Small through holes and blind holes
- Cross holes and angled holes
- Thin walls in suitable geometry
- Grooves, small slots, and side features
- Undercuts where tooling design allows release
- Fine teeth, splines, or molded functional details
- Part consolidation from multiple machined or assembled parts
- Repeatable small features over medium-to-high-volume production
The Metal Injection Molding Association notes that MIM can offer advantages over investment casting in thinner wall sections, sharper features, small-diameter holes, improved surface finish, reduced finish machining, and high volumes of small components. See MIMA design guidance.
Where Investment Casting Still Works Well
Investment casting remains effective for complex cast geometries, larger metal parts, organic contours, thicker sections, and shapes that are not suitable for injection molding and sintering economics. It can also be appropriate when the part geometry is complex but does not contain many micro-features that need MIM-level molding repeatability.
In production, this usually depends on whether the complexity is “casting complexity” or “small precision feature complexity.” A curved cast body may be a good investment casting candidate. A small part with multiple tiny functional features may be a better MIM candidate.
Design Review Warning: Casting Geometry Cannot Always Be Moved Directly to MIM
A common mistake is to take an investment casting drawing and ask for direct MIM production without redesign. This can create avoidable tooling and quality risks.
Before moving from investment casting to MIM, engineers should recheck:
- Wall thickness uniformity and thick-to-thin transitions
- Gate location, parting line, and ejection direction
- Debinding path and risk of trapped binder
- Sintering support direction and distortion risk
- Shrinkage compensation and datum strategy
- Critical functional surfaces and machining allowance
- Whether cast radii, bosses, ribs, or heavy sections need redesign
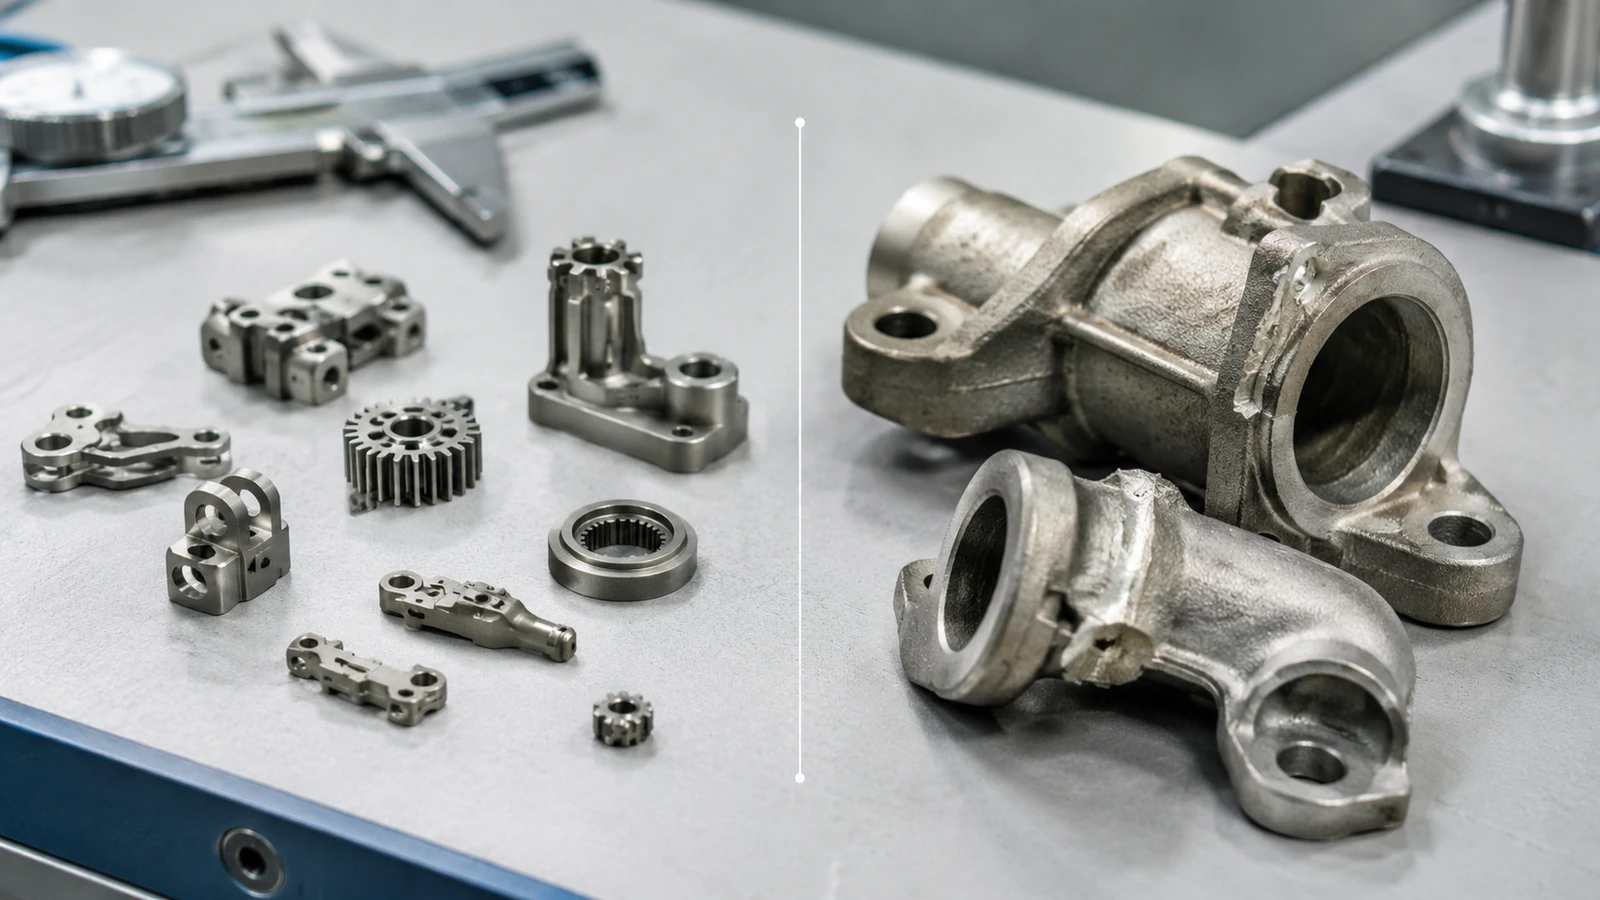
Material Selection: MIM Powders vs Cast Alloys
MIM Materials Should Be Selected by Powder Availability and Sintering Behavior
MIM material selection depends on more than alloy name. The material must be available as suitable powder, compatible with feedstock preparation, moldable in the selected geometry, stable through debinding, and capable of reaching the required density and properties after sintering and any secondary operations.
Common MIM material families may include stainless steels, low alloy steels, tool steels, soft magnetic alloys, tungsten alloys, cobalt-chromium alloys, and selected titanium alloys where the supplier has proven process capability. However, not every wrought or cast alloy can be assumed to be practical in MIM.
Investment Casting Usually Offers a Broader Casting Alloy Route
Investment casting is widely used for many cast alloy families, including stainless steels, carbon steels, nickel alloys, cobalt alloys, aluminum alloys, copper alloys, titanium alloys, and heat-resistant alloys depending on foundry capability and application requirements.
This is one reason investment casting remains strong in aerospace, defense, energy, medical, and industrial applications. For certain large, high-temperature, or alloy-specific cast components, investment casting may be the more established route.
Do Not Choose Only by Alloy Name
The same alloy family can behave differently in MIM and investment casting. Density, microstructure, heat treatment response, corrosion behavior, magnetic performance, surface condition, and dimensional stability can all depend on the process route.
Material feasibility should be confirmed at the part-and-process level: can the selected MIM route produce the required alloy, geometry, annual volume, critical dimensions, inspection requirements, and operating performance consistently?
Cost and Production Volume: Which Process Is More Economical?
MIM Cost Logic
MIM usually requires higher early engineering and tooling investment than low-volume casting routes. Tooling, feedstock development, molding validation, debinding, sintering, and inspection setup must be justified by the project.
MIM becomes more attractive when production volume is high enough to amortize tooling, when multi-cavity tooling can be used, when expensive machining can be reduced, or when multiple parts can be consolidated into one molded component.
Investment Casting Cost Logic
Investment casting can be more economical when annual volume is lower, part size is larger, or the design is already well suited to casting. It may also be more practical when the project requires a cast alloy route, when initial tooling flexibility matters, or when secondary machining is already expected.
However, investment casting cost should not be judged only by casting price. Ceramic shell production, gating, yield, heat treatment, finishing, machining, and inspection can all affect the accepted final part cost.
Cost Decision Table
| Cost Factor | Better for MIM | Better for Investment Casting |
|---|---|---|
| Annual volume | Medium to high repeat production | Low to medium volume |
| Part size | Small and compact | Medium to large |
| Geometry | Small complex details reduce machining | Cast complexity without many micro-features |
| Tooling amortization | Stronger when volume is high | Better when lower initial investment is needed |
| Material cost impact | More acceptable when part weight is small | Often better for larger cast metal mass |
| Machining reduction | Strong advantage if features can be molded | Machining may still be needed for critical surfaces |
| Final cost logic | Best when finished part cost drops over volume | Best when casting plus finishing remains economical |
Tolerance and Dimensional Control
Why MIM Can Be Strong for Repeatable Small-Part Tolerances
MIM can be strong for repeatable small-part tolerances when the geometry is suitable and the process is well controlled. The injection mold can be designed with shrinkage compensation, and the production process can be tuned around feedstock, molding parameters, debinding, sintering support, and inspection feedback.
This matters for parts with small features and repeated production demand. If the same geometry must be produced consistently over thousands or millions of parts, MIM can become more attractive than a casting route that requires repeated machining or manual finishing.
However, MIM should not be described as automatically tighter for every part. Poor wall thickness balance, unsupported sintering geometry, large mass variation, or unrealistic drawing tolerances can still create quality problems.
Why Investment Casting Often Needs Machining for Critical Dimensions
Investment casting can produce accurate and complex castings, but critical dimensions often depend on the wax pattern, ceramic shell, thermal expansion, metal flow, solidification, cooling, gate removal, and post-casting finishing. For high-precision datum surfaces, sealing faces, bearing fits, or thread interfaces, machining may still be required.
A meaningful cost comparison should include casting, grinding, machining, finishing, inspection, and yield—not only the casting price.
Surface Finish and Secondary Operations
MIM Can Reduce Some Finishing and Machining Steps
MIM can reproduce fine molded details and may reduce the need for machining small features. For suitable parts, features such as grooves, small holes, logos, textures, splines, and complex contours may be molded instead of machined.
MIM secondary operations may still be required depending on the project. These can include heat treatment, sizing, polishing, passivation, plating, coating, CNC machining, or other finishing operations. MIM is valuable when molded geometry removes enough secondary machining to improve the finished-part process, not when every finishing step is expected to disappear.
Investment Cast Parts May Still Need Grinding, Machining, or Surface Finishing
Investment cast parts may require gate removal, shell removal cleanup, grinding, blasting, polishing, heat treatment, machining, or surface finishing. Some surfaces may be acceptable as-cast, while critical features may require post-casting machining.
The Real Comparison Is Total Finished Part Cost
Compare accepted finished-part cost rather than MIM blank price against investment-casting blank price.
- Tooling and process development
- Material and feedstock or cast alloy cost
- Scrap risk and inspection sorting
- Machining and finishing workload
- Heat treatment or surface treatment
- Yield, lead time, and repeatability
- Final functional acceptance, not only the raw blank price
Quality Risks and Inspection Focus: Sintering Distortion vs Casting Defects
MIM Quality Risks: Debinding Cracks, Sintering Distortion, and Shrinkage Variation
MIM quality risks usually come from the interaction between geometry and process control. Common risks include short shots, weld lines, green part handling damage, debinding cracks, brown part fragility, sintering distortion, nonuniform shrinkage, warpage from poor support, dimensional drift across batches, and surface defects after sintering or finishing.
These risks do not mean MIM is unstable. They mean that MIM must be reviewed as a powder-based injection and sintering route, not as a simple replacement for casting.
Investment Casting Quality Risks: Porosity, Shrinkage Cavities, Shell Defects, and Gate Removal
Investment casting quality risks are tied to wax pattern quality, shell building, dewaxing, metal pouring, solidification, and finishing. Typical concerns include wax pattern variation, shell cracks, porosity, shrinkage cavities, inclusions, misruns, gate removal marks, surface imperfections, and machining allowance issues.
The Investment Casting Institute describes shell building as repeated ceramic slurry and stucco coating around the wax tree, followed by dewaxing and metal pouring into the preheated shell. See shell building reference.
What Engineers Should Inspect Before Approving Production
Before approving either process, engineers should define the inspection method, datum structure, functional surfaces, critical dimensions, material condition, heat treatment requirements, cosmetic expectations, and batch-to-batch control expectations.
| Risk Area | MIM Review Focus | Investment Casting Review Focus | Why It Matters |
|---|---|---|---|
| Dimensional variation | Tooling compensation, sintering shrinkage, support method, batch stability | Wax pattern accuracy, shell expansion, solidification shrinkage, machining allowance | Critical dimensions may fail even when the part shape appears correct. |
| Internal defects | Debinding stability, trapped binder, thick section risk, sintering density | Porosity, shrinkage cavities, inclusions, feeding and gating strategy | Internal defects can affect strength, sealing, fatigue, corrosion, or assembly reliability. |
| Surface and finishing | Mold surface, sintering marks, support contact, secondary finishing need | Shell texture, gate removal, blasting, grinding, polishing, machining | Surface condition affects cosmetic acceptance, friction, sealing, and corrosion behavior. |
| Production repeatability | Feedstock lot control, molding parameters, debinding/sintering cycle consistency | Wax assembly, shell drying, pouring temperature, cooling, heat treatment | Repeatability determines whether prototype approval can translate into stable production. |
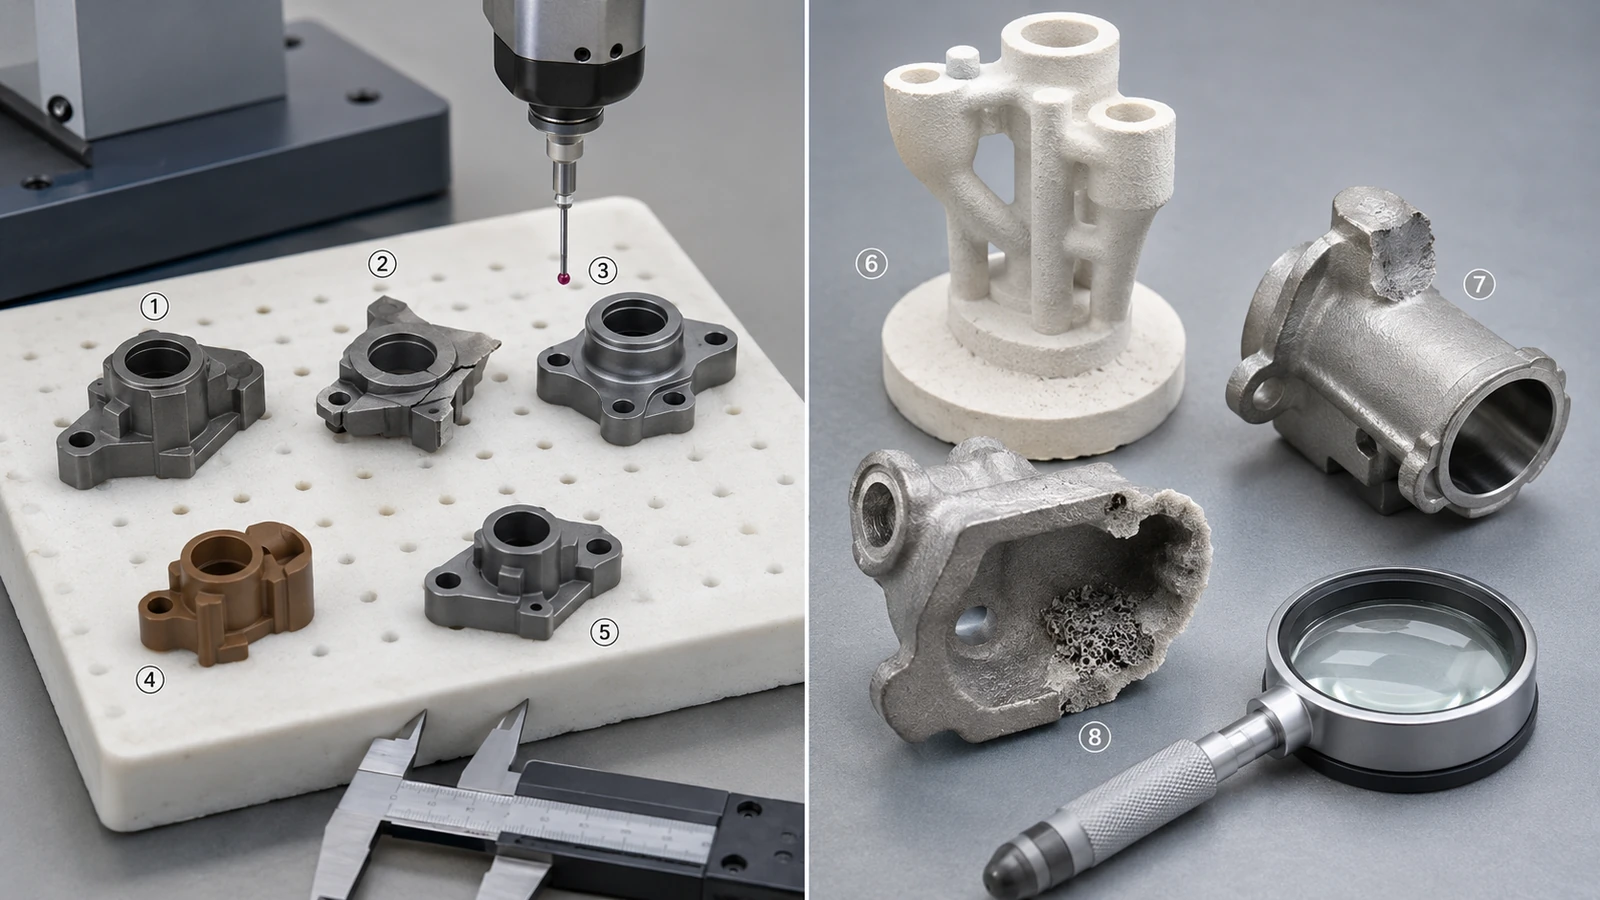
Is Your Investment Cast Part a Good Candidate for MIM Conversion?
When an Existing Investment-Cast Part Deserves MIM Conversion Review
A conversion review is most useful when the current manufacturing route itself creates avoidable cost, variation, or secondary work. Strong signals include:
- Repeated machining, grinding, or finishing is required to create small functional features.
- Dimensional variation or finishing creates recurring inspection, sorting, or rework pressure.
- Multiple components or operations could potentially be consolidated into one molded part.
- Annual demand is stable enough to justify dedicated tooling and process validation.
- The geometry can be redesigned around more balanced wall thickness and sintering support.
- The specified material has a practical, proven MIM feedstock and sintering route.
A strong conversion candidate is not simply a small casting. MIM becomes more compelling when the existing casting route leaves substantial machining, finishing, assembly, repeatability, or total-cost pressure that a redesigned MIM part can reduce.
When Conversion Is Unlikely to Add Enough Value
Keeping the investment-casting route may be more practical when:
- The current casting already meets cost, quality, and delivery needs with little secondary machining.
- Demand is low or unstable, so dedicated MIM tooling and validation cannot be justified.
- The part is large, heavy, or dominated by very thick and uneven sections.
- The required alloy, cast microstructure, or customer specification depends on a casting route.
- Most critical surfaces would still require full machining after MIM.
- The geometry cannot be adapted for MIM gating, debinding, shrinkage control, ejection, or sintering support without compromising function.
What Must Be Rechecked Before Replacing Investment Casting with MIM
Before converting an investment cast part to MIM, recheck the overall part envelope, maximum section thickness, wall thickness variation, internal holes, gate and parting line options, sintering support direction, critical tolerance zones, machining allowance, material availability, production volume, inspection requirements, and application environment.
When an Investment Cast Part Looks Like a MIM Candidate but Needs Redesign
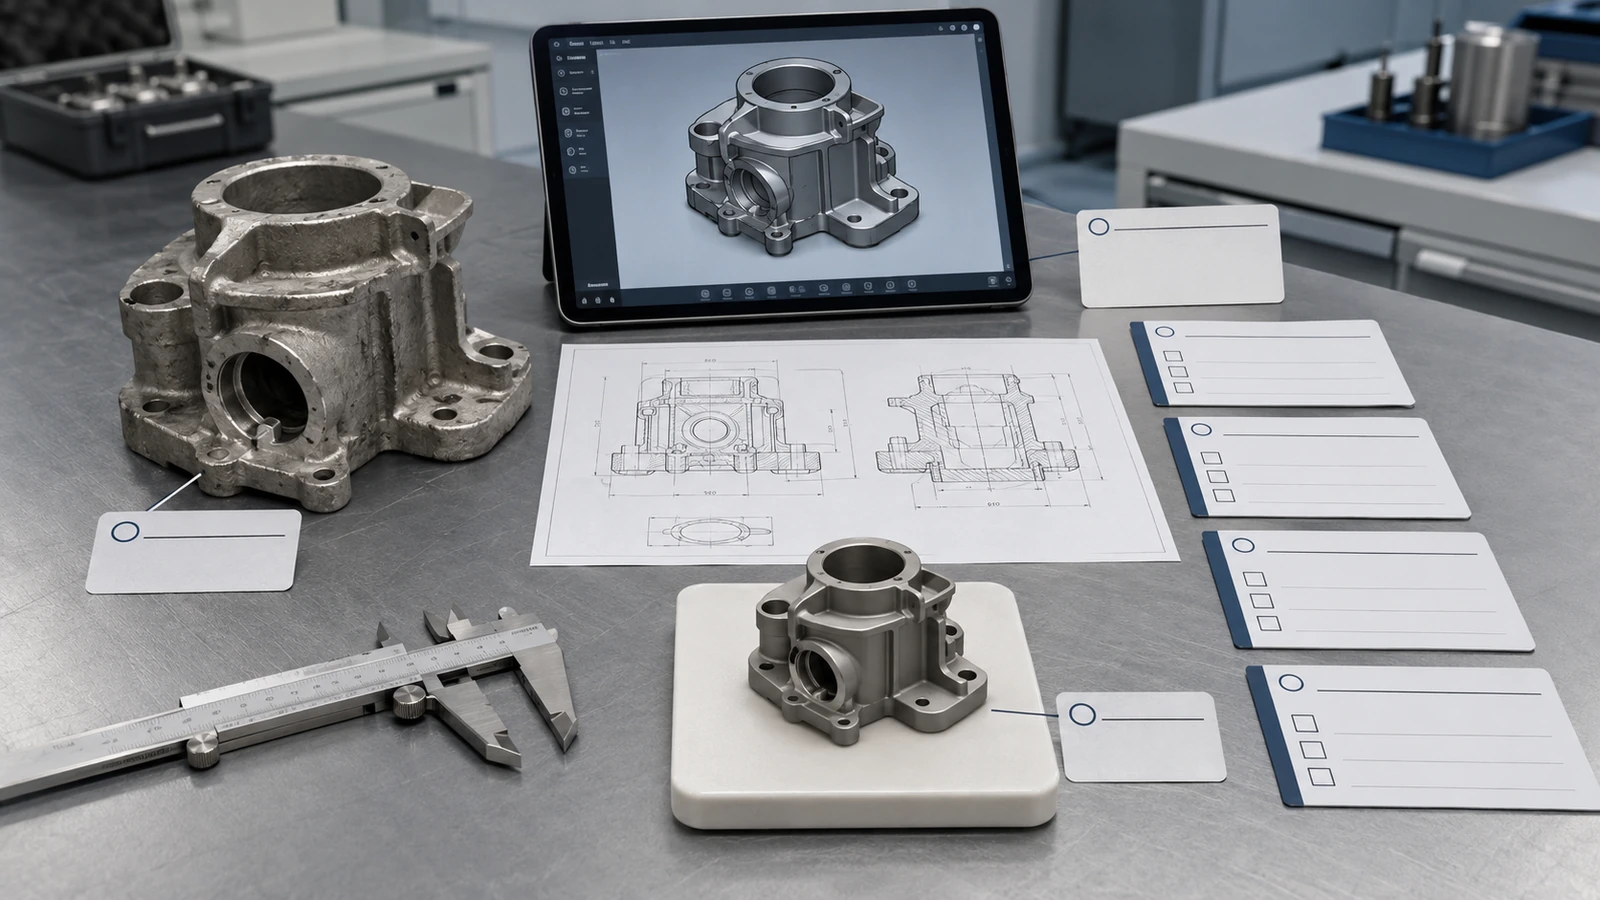
Design issue: a small cast component with several holes and a machined slot can initially look suitable for MIM conversion, yet a thick boss connected to a thin arm and a critical flatness requirement across the longest span can change that assessment.
Why the casting drawing needs changes: the original geometry may work in investment casting because a heavy local section can be filled as molten metal and machined afterward. In MIM, the same mass concentration changes binder-removal behavior, shrinkage balance, and sintering support requirements, increasing distortion risk even though the overall part remains small.
Engineering response: review wall-thickness balance, gate position, support direction, datum strategy, critical flatness, and machining allowance before mold design. Where function allows, reduce non-critical mass or smooth thick-to-thin transitions while keeping functional surfaces tied to a clear inspection plan.
Common Mistakes When Comparing MIM and Investment Casting
Comparing Raw Part Price Instead of Finished Part Cost
A lower casting price may not mean lower final cost if machining, grinding, finishing, inspection, or yield loss is significant.
Assuming All Cast Alloys Can Be Converted to MIM
MIM material selection depends on powder availability, feedstock stability, sintering behavior, final density, and application performance.
Ignoring Section Thickness
A small part with thick sections can still be difficult for MIM because binder removal and sintering shrinkage must remain stable.
Reusing Investment Casting Drawings Without MIM DFM Review
Casting drawings often include geometry, radii, tolerances, and machining allowances that may not be ideal for MIM.
Treating Surface Finish as a Fixed Process Value
Surface finish depends on tooling, material, process control, finishing method, and part geometry.
Ignoring Annual Volume
MIM is often more attractive when volume is high enough to justify tooling and process development.
Drawing Review Checklist Before Choosing MIM or Investment Casting
Before choosing between MIM and investment casting, prepare the following information for supplier review:
- 2D drawing with critical dimensions
- 3D CAD file
- Material grade or required mechanical properties
- Estimated annual volume
- Part weight and envelope size
- Maximum and minimum wall thickness
- Critical tolerance zones
- Surface finish requirements
- Heat treatment requirements
- Corrosion, wear, magnetic, or biocompatibility requirements
- Assembly interfaces
- Functional surfaces
- Existing process pain points
- Current machining or finishing steps
- Target production stage: prototype, trial production, or mass production
A useful RFQ should include the drawing, material requirements, tolerance expectations, annual volume, application background, and any current casting or machining problems that need to be resolved before tooling.
Before Asking for a Quote, Send These 6 Items
To receive a useful process recommendation instead of a rough price guess, send enough information for engineering review. These six items help XTMIM judge whether MIM is technically and commercially suitable compared with investment casting.
- 2D drawing with marked critical dimensions
- 3D CAD file for geometry and moldability review
- Material grade or required performance target
- Estimated annual volume and production stage
- Critical tolerance, surface, and assembly requirements
- Current casting, machining, quality, or cost pain points
The clearer the drawing package, the easier it is to identify whether the part is a strong MIM candidate, a better investment casting project, or a design that needs modification before any process can be quoted accurately.
Need to Know Whether Your Investment Cast Part Can Be Converted to MIM?
Send your drawing, 3D file, material requirement, critical tolerances, surface requirements, and estimated annual volume. XTMIM can review whether the part is suitable for MIM, whether redesign is needed, and which process risks should be checked before tooling, trial production, or mass production.
Standards and Technical References for Process Evaluation
MIM and investment casting decisions should be based on drawings, material requirements, process capability, and inspection expectations. General process references from organizations such as MIMA, EPMA, MPIF, and the Investment Casting Institute can help define the basic manufacturing route and design logic, but they should not replace project-specific engineering review.
When material performance, medical use, aerospace use, corrosion resistance, heat treatment, density, mechanical properties, or inspection acceptance is critical, the final requirement should be confirmed through applicable ASTM, ISO, customer, or industry standards. Do not assume that a general MIM or investment casting comparison automatically defines acceptable tolerance, strength, density, or surface condition for a specific part.
MIM vs Investment Casting FAQs
Can a small investment-cast part still be a poor MIM candidate?
Yes. Small overall size does not guarantee MIM suitability. Very thick or uneven sections, isolated mass concentrations, an impractical material route, low annual demand, or blanket tight tolerances can make MIM difficult or uneconomical even when the part fits easily within a small envelope.
Can the existing investment-casting drawing be sent directly for MIM tooling?
It should be used as a starting point, not treated as a tooling-ready MIM drawing. Wall thickness, thick-to-thin transitions, gate and ejection options, debinding paths, sintering support, shrinkage compensation, datum strategy, critical tolerances, and machining allowance should be reviewed before mold design.
Is MIM still attractive if some critical surfaces require machining?
It can be. The key question is whether MIM removes enough other machining, finishing, assembly, or variation to reduce the accepted finished-part cost. If most critical geometry still requires full machining after sintering, the conversion advantage becomes much weaker.
What information is needed for a useful MIM vs investment casting review?
Provide the 2D drawing, 3D CAD file, material or performance requirement, critical dimensions, part size and section thickness, annual volume, surface and heat-treatment requirements, application conditions, and the current casting, machining, quality, or cost problems you want the new process to solve.