
MIM Watch Parts for Precision Watch Hardware
MIM Watch Parts for Small, Complex and Appearance-Critical Metal Hardware
MIM watch parts are suitable when a small metal component combines complex geometry, repeatable production demand, controlled surface appearance, and assembly requirements that are difficult to achieve efficiently by simple machining or stamping. For watch-related projects, this may include buckles, clasps, strap links, buttons, band adapters, connectors, small internal hardware, and selected case-related parts. Part size alone is not enough to justify MIM. The complete manufacturing route should be checked together: fine metal powder and binder feedstock, injection molding, green part handling, debinding, sintering shrinkage, tooling compensation, secondary finishing, and final inspection. If visible surfaces, coating buildup, gate location, parting lines, material route, tolerance stack-up, and annual volume are not reviewed before tooling, a part can look manufacturable but fail cosmetic or assembly validation later.
Watch cases, housings, frames, bezels, and lugs usually need deeper review because visible surfaces, material choice, finishing allowances, assembly interfaces, and shrinkage compensation interact more strongly than they do on many smaller watch components. For case-specific engineering details, see the MIM watch case parts engineering review.
Key Engineering Questions
- Does the geometry and production demand justify MIM tooling?
- Which material and finishing route fits the part function?
- How could shrinkage, coating, gates, or parting lines affect fit and appearance?
- What drawings, tolerances, cosmetic zones, and volume data are needed before RFQ review?
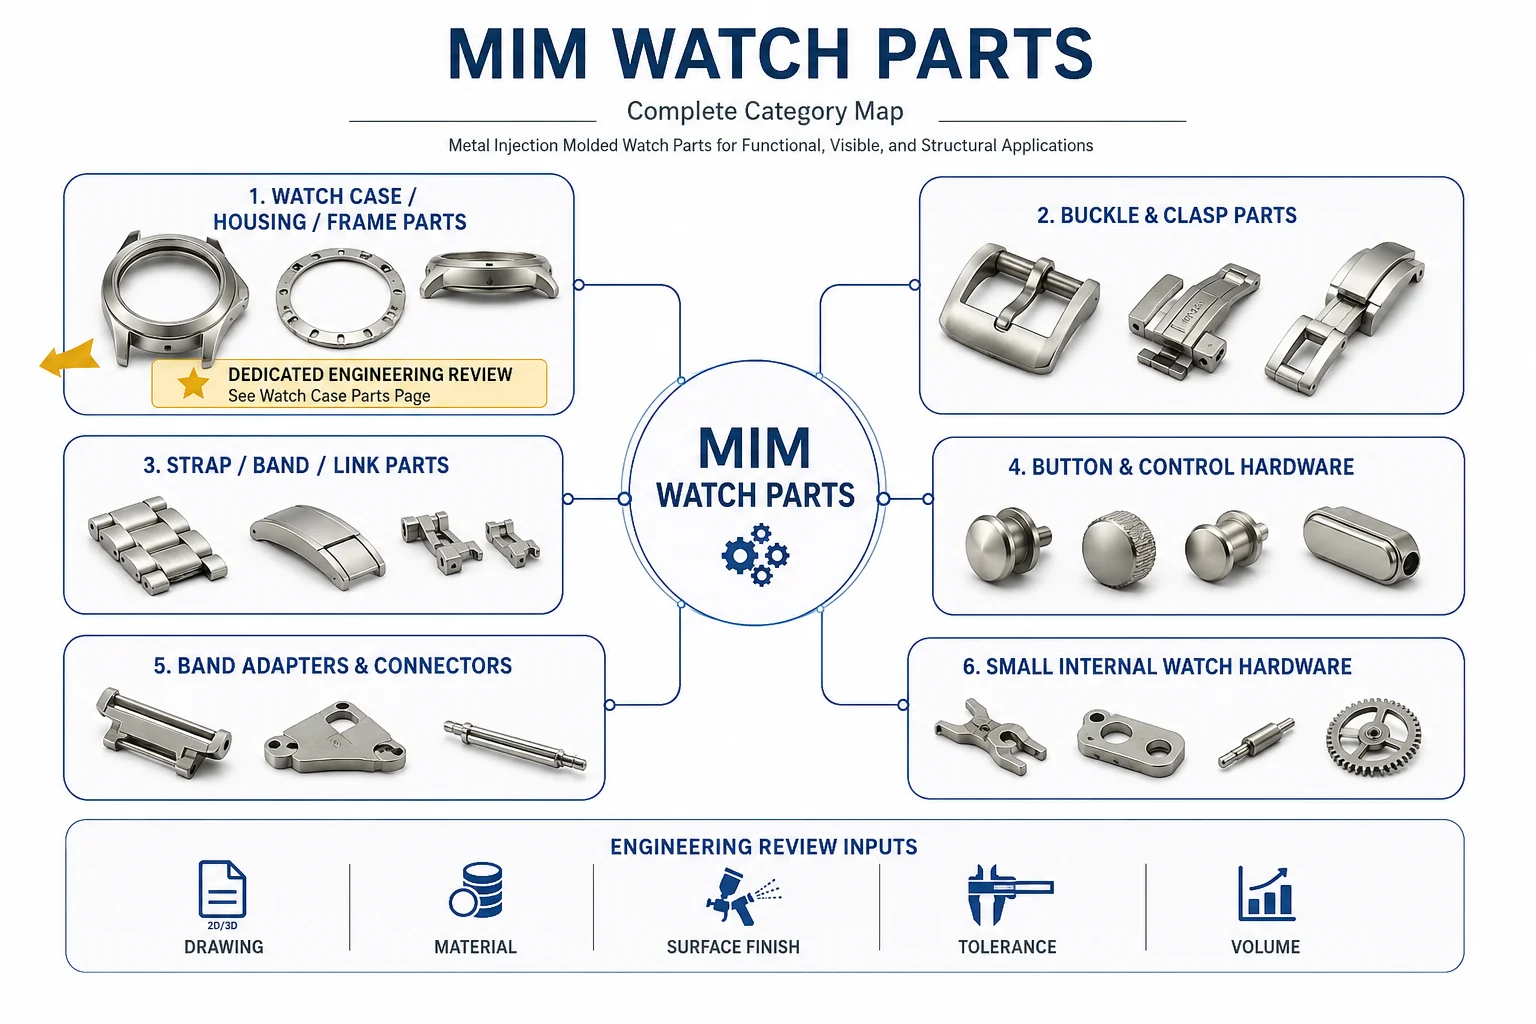
What Types of Watch Parts Are Suitable for MIM?
From a design review perspective, a watch part becomes a stronger MIM candidate when it combines compact size, three-dimensional geometry, repeated production demand, and material requirements that justify tooling. MIM is especially useful when machining would require multiple setups, when stamping cannot create the required geometry, or when casting would not provide the desired small-feature control.
The strongest candidates are not always the most visible parts. In practice, a hidden locking element or connector may be a better MIM candidate than a simple visible cover because it combines load direction, small geometry, and assembly function. A common mistake is to select MIM because a part is small, while ignoring whether polishing, coating, sintering distortion, or tolerance stack-up will affect final fit.

| Watch Part Requirement | Good Fit for MIM | Needs Careful Review |
|---|---|---|
| Small complex geometry | Buckles, clasp arms, buttons, adapters, selected case-related features | Very simple flat stamped parts |
| Repeat production | Custom watch hardware with stable annual demand | One-off luxury repair or replacement parts |
| Visible cosmetic surface | Polished, brushed, plated, or PVD-coated parts with defined cosmetic zones | Surfaces where gate or parting-line planning cannot be accepted |
| Assembly function | Connectors, clasps, buttons, locking parts | Tight movement or fit after coating buildup |
| Material requirement | Stainless steel, selected titanium alloy, selected tungsten alloy projects | Materials without a stable feedstock, sintering, or finishing route |
| Secondary operations | Parts with limited machining or controlled polishing allowance | Parts requiring extensive CNC after sintering |
When MIM May Not Be the Best Choice for Watch Parts
The same suitability review should identify when another manufacturing route is more practical. This helps buyers avoid tooling decisions that look attractive at first but become inefficient during finishing, inspection, or assembly.
Low-Volume Custom or Repair Replacement Parts
MIM is usually not the first choice for one-off watch repair parts, replacement components, or very low-volume luxury customization. Tooling, feedstock control, debinding, sintering, and validation require project investment.
Geometry Too Simple for MIM
If a strap component is a flat plate, a simple stamped shape, or a basic machined profile, MIM may not provide enough value. MIM becomes more useful when it integrates complexity or reduces assembly.
Excessive Machining After MIM
MIM is most attractive when it produces a near-net-shape part. If the part requires heavy machining on most important features after sintering, the cost advantage may disappear.
Uncontrolled Cosmetic Expectations
If the design does not allow a hidden gate area, acceptable parting-line position, or practical finishing route, MIM may require design modification or may not be the best choice.
Typical MIM Watch Parts We Review
Common MIM watch-part candidates include the families below. Final manufacturability depends on drawing details, material, tolerance, finishing, annual volume, inspection requirements, and whether the part can remain near-net shape after sintering.
Watch Case, Housing and Frame Parts
Watch cases, smart watch housings, electronic watch frames, bezels, side frames, lugs, and case adapters are often the most engineering-intensive watch components. They combine visible surfaces, assembly interfaces, material selection, sintering shrinkage compensation, and post-finishing requirements.
Because case components combine housing geometry, bezel and back-cover interfaces, visible surfaces, lugs, material selection, and finishing allowances, review them in more detail in the MIM watch case parts engineering review.
Case-specific review Case-related parts Housing / frameWatch Buckle and Clasp Parts
MIM can be considered for pin buckles, folding clasp parts, deployant clasp components, buckle frames, clasp arms, latch-related features, and strap locking hardware when the geometry is difficult to machine or stamp efficiently.
These parts often combine visible surfaces with repeated movement, so the review should include strength, wear surfaces, polishing allowance, coating buildup, parting-line visibility, and assembly clearance.
Buckle frame Clasp arm Locking featureWatch Strap, Band and Link Parts
Metal band links, end links, decorative strap hardware, side links, strap connectors, and PVD-coated strap components can be MIM candidates when they include complex shapes, integrated decorative features, or repeated assembly interfaces.
For strap and band parts, the review should focus on edge rounding, link-to-link fit, surface consistency, polishing allowance, coating thickness, and inspection after finishing.
Band link End link Decorative hardwareWatch Buttons and Control Hardware
Side buttons, smart watch buttons, push-button metal parts, button caps, button support features, and crown-adjacent metal hardware may fit MIM when the part has small features, compact geometry, and repeatable production requirements.
The crown itself may require machining, knurling, sealing, or different production logic, so not every crown component should be treated as an automatic MIM candidate.
Side button Button cap Control hardwareWatch Band Adapters and Connectors
Band adapters, strap adapters, quick-release connector parts, case-to-band connectors, smart watch connector frames, and small locking connectors can be strong candidates when they combine load direction, compact geometry, and visible or semi-visible surfaces.
The main review questions are load transfer, dimensional stability after coating, hidden gate location, and separation between cosmetic and functional surfaces.
Band adapter Quick-release connector Locking geometrySmall Internal Watch Hardware
Miniature brackets, support plates, compact inserts, small internal metal frames, dense small components, and gear-adjacent support parts may be reviewed for MIM when they are too complex for simple machining or stamping.
If the primary design challenge is better defined by a gear, bracket, shaft or pin, or a high-precision feature rather than by the watch application itself, review the corresponding guides for MIM gears, MIM brackets, MIM shafts and pins, or high precision MIM parts.
Support frame Compact insert Internal hardwareMaterials Commonly Considered for MIM Watch Parts
Material selection for MIM watch parts should be reviewed at the same time as geometry and finishing. A material may be attractive for corrosion resistance, density, weight, or appearance, but the real question is whether the material can be processed consistently through feedstock preparation, injection molding, debinding, sintering, finishing, and final inspection.
Stainless Steel for Watch Hardware
Stainless steel is commonly considered for visible watch hardware because it can support corrosion resistance, polishing, brushing, plating, or PVD-related requirements depending on grade and finishing route.
For deeper material family selection, review MIM stainless steel materials.
Titanium Alloy for Lightweight or Premium Hardware
Titanium alloy may be considered for lightweight or premium watch hardware, but it should be reviewed carefully for feedstock route, sintering control, contamination sensitivity, finishing response, and cost.
Tungsten Alloy for Dense or Weight-Sensitive Parts
Tungsten alloy may be considered for dense or weight-sensitive watch components, selected premium hardware, or balance-related small parts. It is not automatically suitable for every visible part.
| Material Direction | Why It May Be Considered | Review Before Tooling | Watch-Part Focus |
|---|---|---|---|
| Stainless steel | Corrosion resistance and compatibility with polished, brushed, plated, or PVD-finished hardware depending on grade | Grade, feedstock route, shrinkage behavior, finishing sequence, and any skin-contact requirements | Visible hardware, links, clasps, connectors, and selected case-related parts |
| Titanium alloy | Lightweight or premium hardware direction | Feedstock route, sintering control, contamination sensitivity, finishing response, and cost | Parts where low weight and premium material positioning justify the added process review |
| Tungsten alloy | High-density or weight-sensitive component direction | Geometry, feedstock and sintering route, finishing requirements, and whether high density is functionally useful | Dense small parts, selected premium hardware, or balance-related components |
Material selection affects feedstock behavior, shrinkage, sintering support, final density, finishing response, dimensional stability, and inspection planning. Changing material after tooling can affect shrinkage compensation and part quality, so the material route should be confirmed before tooling whenever possible.
For broader material review, visit the MIM materials hub.
When a watch link, clasp, strap connector, case back, or other polished skin-contact component specifically requires a nickel-free stainless steel direction, PANACEA stainless steel for MIM may enter the material shortlist. Material choice alone does not prove compliance; the actual powder or feedstock route, sintering condition, polishing or coating, wear exposure, and finished-part nickel-release validation should still be confirmed before tooling.
Surface Finishing and Cosmetic Requirements for Watch Parts
Watch components are often evaluated not only by dimensions, but also by how they look and feel after finishing. MIM can provide near-net-shape geometry, but many watch parts still require polishing, brushing, grinding, coating, plating, PVD, or localized machining. These finishing steps should be considered part of the manufacturing plan, not a late decoration choice.

Polishing, Brushing and Edge Rounding
Polishing and brushing can remove material and soften edges. This matters for strap links, buckles, clasp arms, buttons, and adapters because the finished part must still assemble correctly after cosmetic work.
PVD, Plating and Coating
PVD, plating, and other coatings can change part thickness and affect moving or mating areas. This is especially important for clasps, buttons, connectors, and quick-release adapters.
Functional Surfaces Are Not Cosmetic Surfaces
A visible buckle surface may need polishing or PVD, while a hidden locking face may need dimensional stability more than gloss. Each surface zone should be mapped before tooling.
DFM Risks That Should Be Checked Before Tooling
MIM watch parts require DFM review before tooling because small visual or dimensional errors can become expensive after molding, debinding, sintering, and finishing. The most common issue is not one single defect, but a mismatch between design expectation and process planning.

| DFM Risk | Affected Watch Parts | Why It Matters | Review Direction |
|---|---|---|---|
| Gate mark on visible surface | Case-related parts, buckles, buttons | Cosmetic rejection risk | Define hidden gate area before tooling |
| Parting line exposure | Clasp frames, adapters, housing-related parts | May become visible after polishing or coating | Confirm parting line position |
| Coating buildup | Clasps, buttons, adapters | Can affect movement or assembly fit | Define coating thickness, masked areas, and final inspection state |
| Sintering distortion | Thin strap hardware, connectors, button parts | Can cause dimensional mismatch | Review wall balance, support strategy, and critical dimensions |
| Polishing allowance loss | Links, buckles, buttons | Can change edges and fit | Reserve finishing allowance and protect functional faces |
| Critical hole shrinkage | Buttons, adapters, connectors | Can affect assembly or pin fit | Define inspection dimensions and post-finish acceptance state |
| Handling damage before sintering | Green parts with thin arms or small features | Green parts are fragile before densification | Review green part handling, tray support, and feature protection |
Inspection Focus After Sintering and Finishing
For watch hardware, inspection should be planned around the final use state, not only the as-sintered part. A component can pass basic sintered inspection but fail after polishing, PVD, plating, or final assembly if the critical surfaces were not defined correctly.
| Inspection Stage | What to Check | Why It Matters for Watch Parts |
|---|---|---|
| After sintering | Shrinkage result, warpage, hole position, thin-feature stability, visible distortion | Confirms whether the MIM route and tooling compensation are stable before finishing. |
| After polishing or brushing | Edge loss, surface waviness, cosmetic consistency, functional surface protection | Polishing can improve appearance but also change dimensions or soften assembly edges. |
| After PVD, plating or coating | Coating buildup, moving fit, masked areas, color consistency, contact surfaces | Coating thickness can affect clasps, buttons, adapters, and other mating features. |
| Final assembly state | Pin fit, button travel, clasp movement, strap connection, visual acceptance surfaces | The final part must satisfy both cosmetic inspection and assembly function, not only dimensional checks. |
What Information Should Buyers Provide for a Watch Parts RFQ?
A useful RFQ should help the engineering team evaluate manufacturability, not only price. For MIM watch parts, the drawing package should show part function, material expectation, cosmetic requirements, tolerances, annual volume, and project stage.
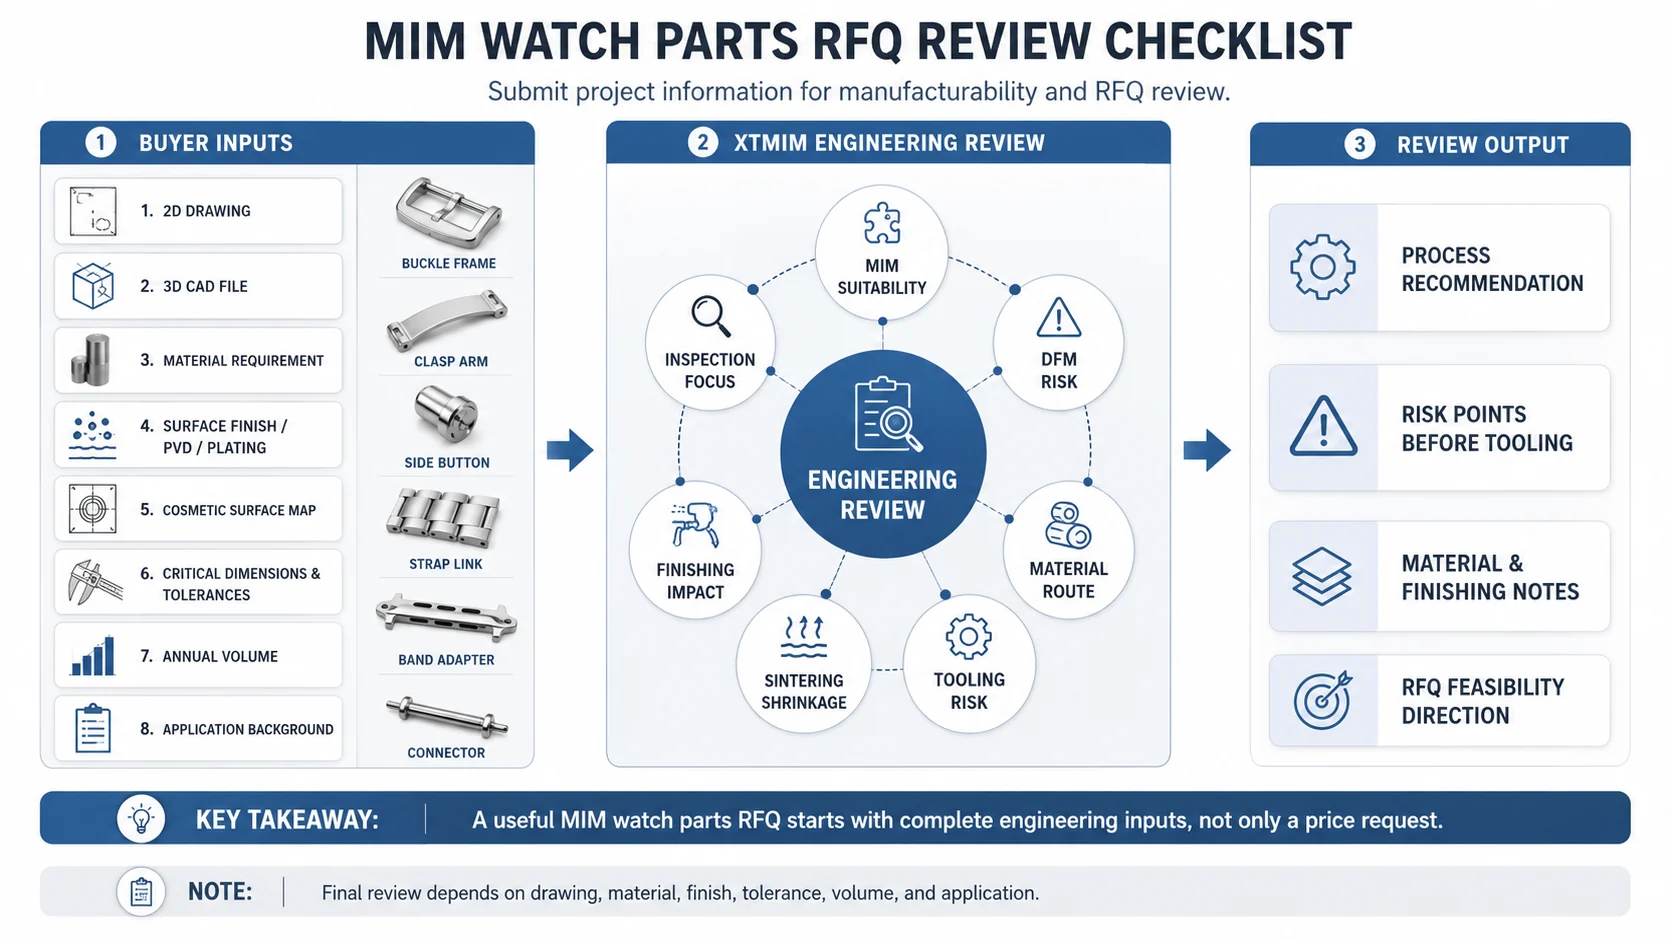
Drawings, 3D Files and Critical Dimensions
- 2D drawing
- 3D CAD model
- Critical dimensions
- Assembly areas
- Hole, slot, pin, or locking features
- Tolerance and inspection requirements
Material, Finish and Cosmetic Requirements
- Target material or material family
- Polishing, brushing, grinding, plating, PVD, or coating
- Visible cosmetic surface map
- Functional contact surfaces
- Masked or protected areas
- Color or gloss expectations if relevant
Application, Volume and Project Stage
- Part type and application background
- Mechanical watch, electronic watch, smart watch, strap hardware, or connector assembly
- Estimated annual volume
- Prototype, trial production, or production stage
- Target assembly function
- Sample photos or existing part references
Send Your Watch Part Drawings for MIM Review
For custom watch buckles, clasp parts, strap links, side buttons, band adapters, connectors, small internal hardware, or case-related MIM parts, send your 2D drawings, 3D CAD files, target material, cosmetic surface requirements, finish expectations, critical dimensions, tolerance needs, annual volume, and application background.
XTMIM can review process suitability, DFM risks, material route, tooling compensation, sintering shrinkage, finishing impact, assembly fit, and inspection focus before tooling or trial production.
Technical References for MIM Watch Parts
Metal injection molding design and material decisions should be guided by recognized technical references, but association materials and standards should not replace project-specific DFM review. For watch parts, the most relevant references are those that explain MIM process capability, material behavior, process economics, skin-contact material evaluation, and suitability for complex small parts.
MIMA: What Is MIM?
The Metal Injection Molding Association explains MIM as a process for complex metal parts that may otherwise require machining or assembly, including why geometry complexity and production repeatability matter in process selection.
EPMA: Metal Injection Moulding
EPMA describes MIM as a route for complex-shaped parts in higher quantities and also explains when simpler manufacturing routes may be more economical.
PIM International: Watch Applications
PIM International documents MIM use in watch-related applications, including case geometry, appearance, material, and production considerations. Final suitability still requires project-specific DFM evaluation.
Coatings Research: Stainless Steel Watch Links
Research on MIM stainless steel watch links provides corrosion and nickel-release data relevant to skin-contact material evaluation. It does not establish suitability for every watch-part design or finishing route.
FAQs About MIM Watch Parts
What watch parts can be made by MIM?
MIM can be considered for watch buckles, clasp parts, strap links, side buttons, band adapters, connectors, small internal metal hardware, and selected case-related parts. Final suitability depends on part geometry, material, visible surfaces, tolerance requirements, finishing route, and annual production volume.
Are MIM watch parts only used for watch cases?
No. Watch cases are only one group of MIM watch components. Buckles, clasps, strap hardware, buttons, adapters, connectors, and small functional components may also be suitable when their geometry, material route, finishing, volume, and assembly requirements fit the MIM process.
Why do watch case parts need deeper engineering review?
Watch case parts combine housing geometry, visible surfaces, material selection, polishing, PVD or coating, lugs, button openings, bezel and back-cover interfaces, and sometimes different requirements for mechanical, electronic, or smart watch designs. These interactions make case components more sensitive to tooling compensation, finishing allowances, cosmetic zoning, and final assembly fit.
Can stainless steel, titanium alloy, or tungsten alloy be used for MIM watch parts?
These materials may be considered for MIM watch parts, but suitability depends on the part design, feedstock availability, sintering behavior, finishing process, cost target, and inspection requirements. Stainless steel is often considered for corrosion-resistant visible hardware; titanium alloy may be reviewed for lightweight premium parts; tungsten alloy may be reviewed for dense or weight-sensitive components.
Do MIM watch parts need corrosion or nickel-release review for skin-contact applications?
Yes. Watch links, buckles, strap connectors, case backs, and selected housing-related parts may contact skin or sweat for long periods, so corrosion behavior, coating durability, nickel-release risk where relevant, cleaning exposure, and final market acceptance requirements should be reviewed before production. Material selection should be confirmed by the specific part design, surface condition, finishing route, and application environment.
Are MIM watch parts ready to use after sintering?
Not always. Many watch parts require polishing, brushing, grinding, coating, plating, PVD, localized machining, or final inspection after sintering. These secondary operations should be considered during DFM review because they can change dimensions, edge condition, surface appearance, and assembly fit.
When is MIM not suitable for watch parts?
MIM may not be suitable for one-off repair parts, simple stamped geometry, very low-volume custom components, parts requiring extensive machining after sintering, or cosmetic designs that cannot accept practical gate, parting-line, polishing, or coating planning.
What information is needed for a MIM watch parts quotation?
A useful RFQ should include 2D drawings, 3D CAD files, target material, surface finish requirements, cosmetic surface map, critical dimensions, tolerance requirements, annual volume, project stage, and application background. Sample photos or existing part references can also help clarify cosmetic and assembly expectations.