
MIM Drawing & DFM Questions Quick Answer Not every MIM shaft or pin needs secondary grinding. The decision depends on function of each cylindrical surface, the required roundness, straightness and runout, and the geometry that remains stable after sintering and any heat treatment. A two-point diameter reading cannot verify every geometric requirement. A clearance body …
Quick Answer
Not every MIM shaft or pin needs secondary grinding. The decision depends on function of each cylindrical surface, the required roundness, straightness and runout, and the geometry that remains stable after sintering and any heat treatment. A two-point diameter reading cannot verify every geometric requirement. A clearance body may remain as-sintered, while a short sliding or bearing journal may need selective grinding. If the entire pin is bowed, however, grinding one journal will not necessarily correct the problem. Before tooling, identify the functional surfaces, assess sintering support and asymmetric features, confirm grinding stock and datum references, and agree on how the finished part will be inspected. Precision finishing should be limited to the surfaces that actually determine fit and motion.
Related page: For typical shaft and pin geometries, materials and manufacturing inquiries, see MIM shafts and pins. The choice between as-sintered and ground surfaces should follow the actual mating function and final inspection requirement.
01 / Identify the requirement
Which Geometric Requirements Matter for Different MIM Shaft and Pin Surfaces?
A stepped MIM pin has a molded head, cross hole, non-contact body and a short sliding journal. Its measured diameter meets the drawing, yet the pin binds in its guide. Before specifying grinding stock, the engineer needs to ask “Which feature controls the assembly, and which characteristic of that feature is failing?” The answer could lie in the pin’s cross-sectional form, its straightness, the mating bore or the way the assembly locates the two parts.
A shaft drawing may control diameter, roundness, straightness, cylindricity, runout and surface texture. These requirements answer different questions about fit and motion; specifying all of them on every surface adds inspection work without necessarily improving function. Their interpretation also depends on the governing drawing standard. General MIM size planning is covered in the MIM tolerances guide; here the focus is the cylindrical features that control assembly.
Identify Functional and Non-Critical Cylindrical Zones
Map the cylindrical surfaces according to what they do in the assembly. Identify the regions that locate, rotate, slide, seal or transfer load, then distinguish them from the body sections that only provide clearance or connect features. An as-sintered surface still needs a defined acceptance condition; it simply may not need the same form or finish requirement as a bearing journal.
AGeneral bodyClearance / exterior
BLocating featureShoulder / positioning
CCritical journalSliding / rotation
Illustrative feature map only. Actual functional zones, datums and tolerance callouts must follow the customer’s part drawing and mating assembly.
| Surface / feature | What the assembly needs | Typical requirement to review | First engineering question |
|---|---|---|---|
| Clearance body, non-contact diameter | Space or an external envelope | Size at defined locations; clearance or envelope | Can the qualified as-sintered state provide the needed clearance? |
| Short locating or press-fit zone | Repeatable location or interference | Size variation, mating-part tolerance, local form | What fit range is functionally acceptable at assembly? |
| Sliding journal | Stable sliding, friction and wear behavior | Size, roundness / cylindricity as justified, texture | Could local high spots or roughness cause binding? |
| Rotating journal | Reliable rotation about a functional axis | Size and form; runout relative to a specified datum when needed | What axis does the bearing or fixture establish? |
| Long guide section | Alignment over an engaged length | Straightness of the specified element or axis; fit | Is full-length bow or only local fit the concern? |
| Shoulder, seal or datum interface | Axial position or controlled contact | Appropriate geometric relationship and surface condition | Which interface actually locates or seals the assembly? |
Match Size, Roundness, Straightness, and Runout to Function
Diameter describes feature size. Roundness addresses the circular form of a section. Straightness can refer to a surface line element or a derived axis, depending on the drawing definition. Cylindricity addresses the form of the cylindrical surface over its specified extent; runout evaluates surface variation in relation to a designated datum axis. Surface texture is separate again, though it may strongly affect wear and sealing.
A two-point micrometer or caliper gives local size information, not a complete description of circular form or runout. That does not mean size limits have no effect on form: ASME and ISO drawing systems differ in their default rules, and drawing notes may modify the interpretation. Apply the standard used on the customer drawing, then select a measurement method that verifies the actual functional characteristic.
Example 1: A pin passes diameter inspection but binds in a guide. Several two-point diameter readings show no obvious size problem, but the pin catches at particular rotational positions. Possible causes include a lobed pin section, an out-of-form mating bore, burrs, surface damage or incorrect assembly alignment. None of these can be identified reliably from a few diameter readings alone.
Inspection sequence: Inspect the mating bore and contact marks first. Measure the pin’s circular profile at the engaged sections with a suitable form method, then repeat the fit test under the specified assembly condition. If the pin’s sectional form is responsible, assess molding or sintering adjustments and, where justified, local journal finishing. If the bore or assembly alignment is responsible, grinding the pin may leave the problem unchanged.
Mitutoyo’s discussion of roundness evaluation methods explains why certain diameter and V-block arrangements can miss particular cross-sectional form errors. A suitably evaluated radial profile can reveal deviations that a two-point check does not. For a tight journal, the measurement method therefore needs to match the specified form characteristic and its intended function.
Drawing requirement: Identify each functional cylindrical surface on the drawing, including its mating role, controlled length, geometric requirement and datum reference where applicable. This information is needed before choosing a finishing operation or assigning grinding stock.
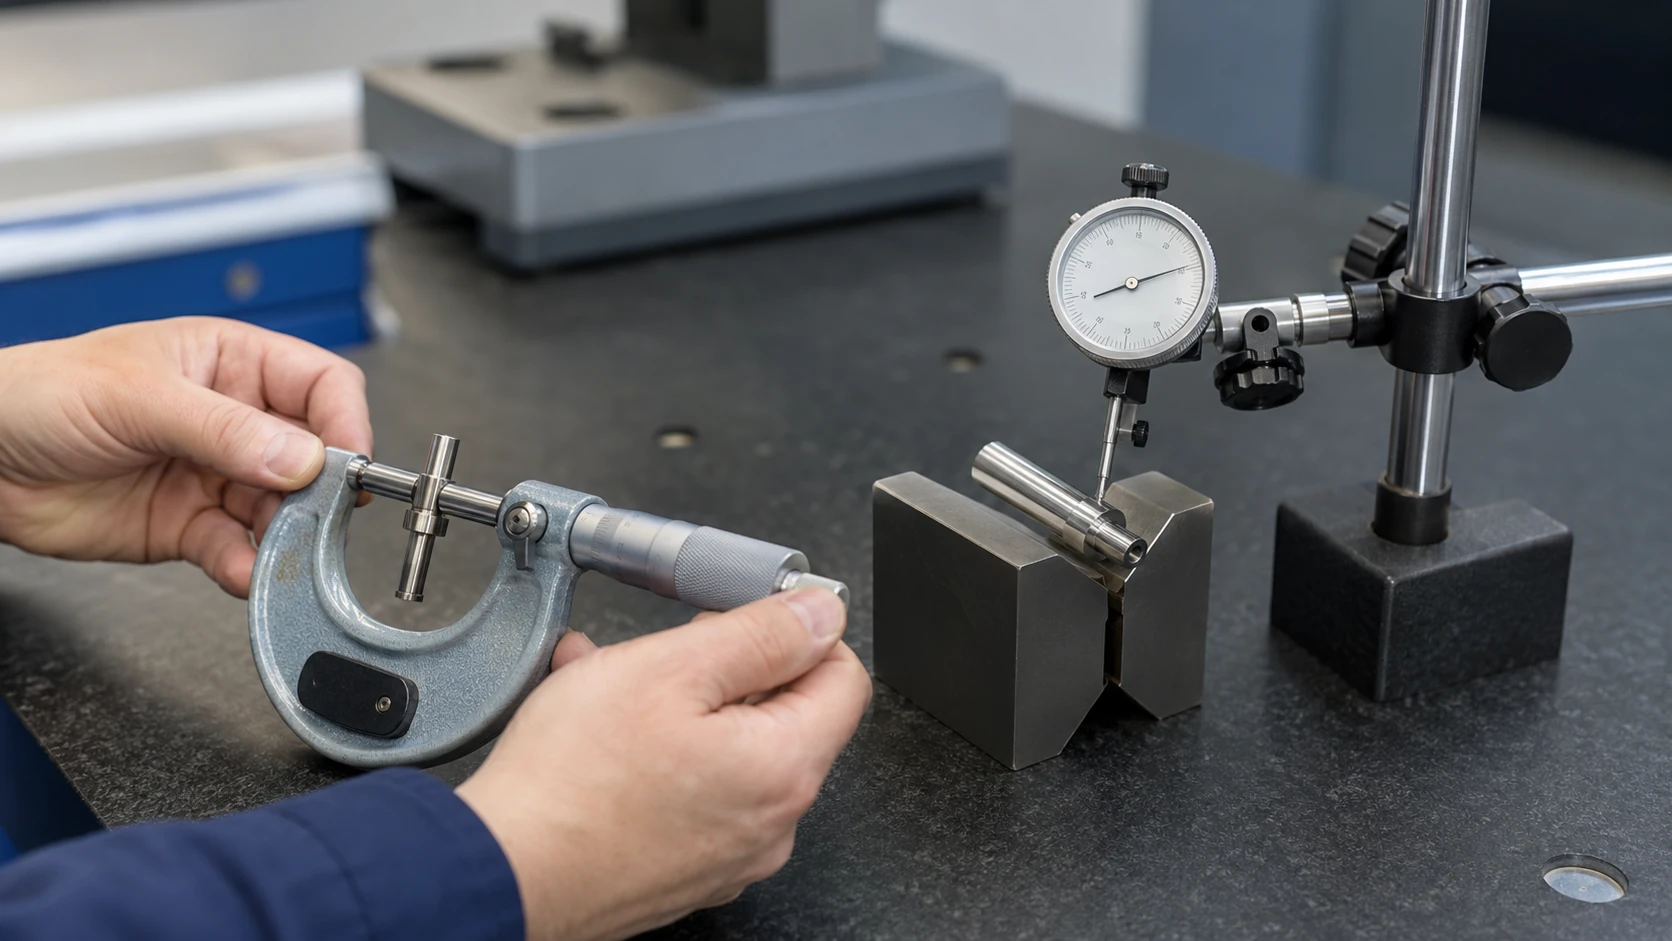
Inspection limit: A passing diameter check does not establish every form or datum-related requirement. Inspection must follow the characteristic shown on the drawing.
02 / Find the variation source
What Causes Roundness and Straightness Variation in MIM Shafts and Pins?
Roundness and straightness can change during molding, debinding, sintering and later heat treatment. Tooling compensation may address a predictable, repeatable size shift, but it cannot reliably remove variable bow or local form error. For a shaft or pin, the critical questions are where the shape changes, how the part is supported and whether the affected region is needed for assembly.
Slender Geometry and Unsupported Spans
Long, slender green parts are more sensitive to handling and support than short, compact parts. During debinding and high-temperature sintering, a long unsupported span may lose its intended shape, particularly when the mass or contact conditions are uneven. The sintering support strategy should therefore be considered during DFM, while the molding orientation and contact surfaces can still be adjusted.
Length-to-diameter ratio is a useful warning sign, not a universal acceptance limit. Two parts with the same ratio may behave differently because of a heavy head, a cross hole, a stepped wall or different setter contact. Specify the length whose straightness matters to the assembly, review the available support points and verify the result on representative parts.
Measure the same controlled straightness feature at defined points in the process. If the part is already bowed after sintering, investigate green handling, support, molding geometry and furnace conditions. If straightness changes chiefly after heat treatment, investigate that operation and its fixturing before changing the mold. Use the same feature definition and comparable support during each measurement; otherwise the apparent process change may come from the inspection setup.
The Metal Injection Molding Association’s design guidance discusses long spans, cantilevers and delicate geometries that may need part-specific sintering supports. For a slender pin, this means checking the actual setter contact and unsupported length rather than assuming a fixed maximum length-to-diameter ratio.
Stepped Features, Cross Holes, and Asymmetric Geometry
A molded head, shoulder, flat, groove or cross hole can eliminate a separate machining or assembly operation, but these features also alter local section geometry. In a stepped shaft, a thick head and thin stem may respond differently to processing, while a cross hole or shoulder may interrupt the surfaces available for sintering support or finishing. The resulting form and datum relationships need to be checked as a complete part.
The same feature can create different risks depending on location. A cross hole near a thin stem, for example, can complicate support or reduce the uninterrupted length available for gripping during grinding. Whether either effect matters depends on the drawing and the chosen route. See how part dimensions affect MIM part quality for the wider relationship between part geometry and MIM dimensional stability.
Example 2: Straightness deteriorates after heat treatment. In this illustrative case, the guided section meets its straightness requirement after sintering but fails after a later heat-treatment cycle. The changed process state suggests examining thermal support, restraint and material response before blaming the mold cavity.
Verification: Compare the same controlled straightness feature immediately after sintering and after heat treatment, with consistent support and inspection methods. If the change is repeatedly associated with the later cycle, review its support and the proposed process sequence. Consider straightening only when the alloy condition, part geometry and subsequent verification make that route feasible; grinding away the bend is not a substitute for this assessment.
Molding, Sintering, and Post-Treatment Repeatability
Gate position, parting lines and ejection features also matter when they coincide with a locating diameter or future ground journal. A witness mark on a bearing surface may require moving the gate, changing the functional area or leaving stock for finishing. Tooling compensation is useful for repeatable shrinkage, but variable distortion first requires a more stable molding and sintering process.
The European Powder Metallurgy Association’s MIM overview describes the substantial shrinkage involved in MIM and the difficulty introduced by varying wall sections. A stepped shaft therefore needs more than a nominal overall shrinkage factor: check the transitions between diameters and confirm that the critical feature relationship is repeatable after sintering.
For heat-treatable materials, specify the required final condition before fixing the finishing sequence. A journal that passes size and form inspection after sintering can change during a later thermal cycle. The risk table distinguishes the observed deviation from its possible causes and the measurements needed to identify the responsible operation.
| Observed or anticipated concern | First possible contributors | DFM action | Evidence needed |
|---|---|---|---|
| Whole-part bow or straightness variation | Slender span, handling, sintering orientation / support, thermal treatment | Review support contact, controlled length and downstream operations | Straightness measurements in specified process states |
| Local circular-form variation | Local geometry, molding / sintering effects, surface interruptions | Review critical section and surface condition | Form measurements at functional sections |
| Runout between a journal and another feature | Datum interpretation, geometry change, finishing setup | Establish functional datum and manufacturing datum relationship | Datum-referenced inspection after finishing |
| Post-heat-treatment loss of fit | Changed part condition or thermal distortion | Reconsider when the final journal is established | Before / after process comparison at critical features |
Design implication: Length, mass distribution and support—not nominal diameter alone—determine which form risks deserve trial inspection.
03 / Select the manufacturing route
When Should MIM Shafts and Pins Stay As-Sintered or Receive Secondary Grinding?
Grinding is a selective solution to a defined functional requirement, not the default final step for every MIM shaft. Start by identifying which surfaces can meet their function as-sintered and which require additional control of size, form or texture. Local form error, full-length bow and datum-related runout are different problems; each needs a finishing or correction method that addresses its actual cause.
Keep Suitable Non-Critical Surfaces As-Sintered
A body diameter used only for clearance may remain as-sintered when samples demonstrate the required fit and repeatability. Some short locating regions may also meet their requirements without finishing. The acceptance criteria must still describe the needed size, envelope or geometric relationship; an area should not be left unchecked simply because it is called non-critical.
On the stepped-pin example, the body between the head and sliding journal may be left as-sintered if it does not guide, locate or interfere with the mating part. The short sliding journal should be evaluated separately for clearance, form and surface texture. This keeps the near-net-shape benefit where it is useful without assuming that every molded surface is suitable for precision contact.
What Selective Grinding Can—and Cannot—Correct
Localized cylindrical grinding can establish the final journal diameter, improve accessible circular form and produce a controlled surface texture when stock, support and machine setup permit. It may also help achieve a specified datum relationship if the setup references the correct features. Grinding the journal alone does not guarantee that an already bent shaft becomes straight, nor does it align an untreated shoulder, cross hole or opposite diameter with the newly ground surface.
A grinding machine generates the finished surface relative to the way the workpiece is held and moved. That setup may differ from the assembly’s datum axis. If a slender pin bends under clamping, it can be ground accurately while restrained and then spring back after removal. Likewise, a round journal can still fail runout relative to a different cylindrical datum. Check workholding deflection, datum simulation and the free-state part after grinding, not just the diameter measured in the fixture.
Grinding stock must cover the clean-up envelope around the entire journal. Eccentricity or local distortion relative to the grinding setup can require unequal removal around the circumference; nominal diameter oversize may therefore be insufficient. Confirm stock on actual sintered or heat-treated samples before freezing the allowance in the tooling design.
A pin with a bowed central body may still acceptably use a short ground journal if the bowed region has only a clearance function. If the assembly guides the full shaft length, however, that bow may remain a failure even after the journal is round. Similarly, a journal ground from the wrong reference surface can meet size and form limits while failing the specified runout.
Grinding may improve
- Local final journal size
- Roundness / local cylindrical form, when the setup supports it
- Surface texture on an accessible functional zone
- Some datum-related relationships, if deliberately established and verified
Grinding does not automatically fix
- Full-length bow or axis straightness outside the ground region
- Unstable sintering or heat-treatment variation
- Misaligned untreated features
- Inadequate fixturing, insufficient stock or an incorrect inspection datum
Choose the grinding method around the actual journal geometry. Centerless grinding can suit certain continuous cylinders, while a stepped or headed pin, interrupted surface or short journal may require a different fixture or grinding process. The setup also has to preserve any specified relationship to the assembly datum axis.
Example 3: Ground journal roundness improves, but runout still fails. A journal is finished using an outer body diameter as the holding reference, but the drawing defines the rotational datum from another locating cylinder. The ground journal improves in roundness yet remains misaligned to the specified datum axis, so runout still fails.
Check before grinding again: Confirm the drawing’s datum feature and the runout inspection setup, then compare the supported and unrestrained part. Correct the fixture reference or process alignment if needed. Removing more material from the journal is unlikely to solve a datum mismatch on its own.
When Sizing, Straightening, or Local Machining May Be More Suitable
Where the main need is a repeatable local size adjustment rather than a fine journal finish, sizing or a suitable form-correction method may be worth testing. Overall bow may call for controlled straightening, provided the material state and geometry allow it. Local turning or grinding can address a designated diameter or shoulder. Select the operation according to the type of error and its acceptable final condition.
Each route has limits. Sizing is not proof of tight roundness or full-axis straightness; straightening needs its own process validation and may affect other features; turning may not deliver the required form or finish without an appropriate setup; and grinding needs sufficient local allowance, accessibility and a compatible datum. Where several options appear feasible, validate the proposed sequence on representative samples before making a production capability claim.
The EPMA identifies grinding, lapping and burnishing among methods that can improve MIM surface finish. Select the method from the journal’s sliding, sealing or wear function; a finer finish alone will not compensate for incorrect form, material or surface treatment. Agree on the required texture and how it will be measured.
When Extensive Finishing Makes the MIM Route Worth Reconsidering
MIM is most useful for a shaft that integrates geometry such as a head, cross hole, flat or groove that would otherwise add machining or assembly steps. Its advantage is less certain for a simple pin requiring precision finishing over nearly its whole length or several separate journal setups. Compare tooling, molding, sintering, treatment, finishing, inspection and expected volumes with turning or another feasible route. The post-sintering machining for MIM parts page covers secondary process choices in more detail.
Published industry example: The MIMA stainless-steel shaft assembly case study describes a 17-4 PH component made through an integrated MIM route with additional joining and precision operations. It shows that near-net-shape forming and finishing can be combined when function requires them. The published case is independent industry evidence, not a statement of XTMIM’s production results or a general requirement to grind MIM shafts.
| Route | When to consider it | What it addresses | What it does not prove | Evidence before tooling |
|---|---|---|---|---|
| A. As-sintered | Surface only needs functionally appropriate size or clearance | Avoids unnecessary finishing of near-net-shape areas | Unmeasured roundness, straightness or runout | Process-capability samples and mating clearance check |
| B. Controlled correction / machining | Localized size or correctable geometry issue | Selected dimensions or geometric errors within the specific process capability | All other geometric requirements without separate validation | Trial route, material state, fixturing and post-operation inspection |
| C. Selective grinding | Critical accessible journal or fit needs a controlled final surface | Local size, form or texture with an appropriate setup | Automatic straightening of the full part or untreated features | Stock, datum, access, sequence and final form/runout measurement |
| D. Alternative process review | Simple full-length precision pin or excessive finishing burden | Potentially simpler full-route production | Lower cost without a volume-and-process comparison | Complete alternative quotes, risk and batch/annual-volume assumptions |
Process selection: Separate local size or roundness error from full-length bow, datum-related runout, texture requirements and production cost. The chosen process must be capable of correcting the identified problem, and its result must be measurable in the final condition. For the cost consequences of added finishing operations, see how secondary operations affect MIM RFQ cost.

Finishing rule: A stepped shaft can contain both as-sintered and finished surfaces; the drawing and the functional inspection decide which ones need machining.
04 / Plan the process before tooling
How Should Grinding Allowance, Datums, and Process Sequence Be Planned Before Tooling?
The chosen finishing route has to be practical before the mold is released. A short journal may need extra stock, but that stock is useless if the part cannot be gripped without bending, the grinding wheel cannot reach the surface, or the finishing fixture cannot preserve the required datum relationship. Review these constraints together with sintering support and the intended final material condition.
Align Functional, Finishing, and Inspection Datums
The functional datum establishes the reference needed for the specified assembly relationship. The manufacturing or finishing datum is the surface or feature combination used to locate the part during material removal. The inspection datum is the reference used to demonstrate conformity with the drawing. They need not be identical physical contact surfaces, but the transfer between them must be defined and checked.
A cylindrical locating feature may establish the assembly’s rotational axis, while a shoulder face establishes its axial seating position. When the finished journal has a runout requirement relative to the cylindrical datum, meeting its diameter limit alone is insufficient. The grinding setup must reproduce that datum relationship, or its transfer must be validated by inspection. A shoulder face alone does not establish the rotational axis; its axial position and face orientation are separate requirements where specified.
Check the datum simulator and contact conditions in the actual fixture. Moving support points along a slender shaft can change its deflection and the axis generated during grinding. If the drawing datum cannot be directly contacted, qualify an alternative setup by measuring the completed part against the specified datum system. The fixture’s repeatability matters as much as its nominal design.
Assembly functionWhich feature locates the part?
Finishing setupWhat can the machine hold reliably?
Final inspectionWhich datum verifies the drawing?
The arrows represent a required relationship, not an instruction to use the same physical contact points for all three operations.
Define Local Finishing Allowance and Fixturing Access
Keep grinding stock on the surfaces that need finishing. Too little stock can leave portions of a distorted or eccentric as-sintered journal; too much can increase cycle time, grinding heat or the risk of damaging a thin section. The allowance depends on material condition, sintered variation, part support and the intended grinding method, so it cannot be specified as one universal value.
State whether the allowance is radial stock or diametral oversize, where the finished journal begins and ends, and when the stock dimension is measured. Assess the minimum material available around the full circumference after allowing for eccentricity, form variation and any later thermal movement. The nominal difference between two diameters does not demonstrate that the surface can be completely cleaned up.
During first-article trials, measure the journal’s size and form before finishing, record the actual fixture references, then check the finished profile and remaining material near shoulders or thin walls. Where the wheel cannot clean the full journal without cutting into an adjacent feature, revise the stock, relief geometry or fixture before approving tooling.
Check grinding access at shoulders, grooves and cross holes, particularly where the wheel must enter or leave a short journal. Also verify that clamping or support will not deform the part. A headed pin and a uniform rod may share a nominal diameter but require different grinding setups; both need trials across the expected sintered variation.
Plan Heat Treatment, Grinding, and the Final Dimensional Condition
The finishing sequence depends on the required final material condition. Heat treatment after grinding can alter form; grinding after heat treatment may require a different wheel, removal rate or setup. Plating, coatings and other surface treatments can also alter fit. Set the sequence around the last operation capable of changing a controlled feature rather than applying one order to every alloy.
Use process-state measurements to distinguish a finishing problem from a thermal-process problem. For instance, measure the controlled length and journal relationship after sintering, repeat after any significant heat treatment, then verify again after finishing and after any subsequent geometry-changing surface treatment. If geometry changes after a later operation, inspecting only the ground part immediately after grinding would give a misleading release result. The sequence must be approved for the actual alloy and required final condition, not applied as a fixed recipe.
Intermediate measurements should isolate where variation enters the process. Final acceptance, however, belongs after the last operation that can materially change the controlled feature. If a subsequent thermal or surface treatment could undo an earlier correction, verify its effect before releasing the part.
Before tooling release: Confirm the functional surface map, drawing datums, grinding allowance, access and fixture plan, and final operation sequence. Identify unresolved conditions for first-article trials rather than assuming a general grinding instruction covers them.
- Critical functional zones and as-sintered candidate areas are identified on the 2D drawing.
- The drawing datum is related to realistic finishing and inspection reference features.
- The exact stock-bearing journal length, transition and minimum allowable remaining section are reviewed.
- Molding, sintering support, heat treatment, correction and finishing sequence is agreed in principle.
- The operation that establishes final dimensions and the final inspection state are unambiguous.
A useful drawing review starts before tooling.
Send the mating function, critical journal, datum requirements and planned finishing condition with the drawing. An early drawing review can identify whether the proposed journal can be supported, reached and inspected without changing the part design.
05 / Prove the final condition
How Should Roundness, Straightness, and Runout Be Measured and Accepted?
The final measured condition must meet the applicable drawing requirements in its specified final state. Local size, circular form, straightness and datum-related runout need different forms of evidence. Passing a grinding operation does not establish conformity unless the finished surface is measured using the appropriate requirement and setup.
Match Each Requirement to an Appropriate Measurement Method
A micrometer can verify local diameter, but not the entire roundness profile or the relationship of a journal to another datum feature. Diameter measurements along a shaft may reveal taper or size variation, but do not by themselves prove cylindricity. Use form measurement for the relevant circular or cylindrical geometry, a qualified CMM strategy for appropriate feature relationships, and a datum-referenced rotational setup for the specified runout. Each method needs adequate resolution and uncertainty for the required limit.
For critical roundness, specify where the cross-section is sampled and how its profile is evaluated. The NIST Engineering Statistics Handbook describes roundness measurement using a full 360-degree trace and notes the possible influence of spindle error. The measuring setup, filtering, calibration and evaluation procedure must be suitable for the drawing requirement; a dense trace alone does not establish measurement accuracy.
A V-block and indicator can provide an agreed functional screen, but the reading depends on contact angle, span and the cross-section’s lobing pattern. It is not automatically interchangeable with a trace-based roundness result. A sparse CMM point pattern can likewise miss short-wavelength form error, so the sampling strategy has to match the feature and tolerance.
For straightness, identify whether the drawing controls a surface line element or a derived axis, and measure the specified length. A long, slender pin may sag under its own weight or change shape when clamped. Record the support points, orientation and evaluation method so that two inspection setups do not report different values merely because they restrain the part differently.
Circular runout and total runout are not interchangeable. On a cylindrical journal, circular runout controls the specified circular elements independently at their cross-sections relative to the drawing-defined datum axis. Total runout applies to the entire specified cylindrical surface over its controlled length relative to that axis, addressing cumulative cross-sectional and lengthwise variation. Checking circular runout at only a few axial stations does not by itself establish compliance with a specified total-runout requirement. Both require an appropriate datum reference and evaluation strategy; neither replaces a separate diameter-size check. Interpret the callout under the actual drawing standard and edition.
Example: Circular runout passes, but total runout fails. A journal may meet the circular-runout requirement at individual checked sections while lengthwise variation causes it to fail a total-runout requirement. Circular runout is evaluated at specified circular elements; total runout requires coverage of the entire controlled surface in the required common datum setup. The inspection plan should follow the drawing’s callout and the circular and total runout measurement distinction rather than treating the two checks as equivalent.
| Drawing characteristic | Possible verification approach | What the method does not automatically establish | Important setup agreement |
|---|---|---|---|
| Diameter / local size | Calibrated micrometer, suitable bore/OD gauge, defined locations | Complete circular form or runout | Section locations, contact, temperature and size definition |
| Roundness of a journal section | Validated circular-form measurement at relevant sections | Full-length straightness or another feature’s datum relationship | Section locations, filtering, centering and evaluation method |
| Axis or surface straightness | Qualified form/CMM or other method suited to the specified element | All diameter and runout requirements | Controlled length, extraction strategy and support conditions |
| Cylindricity | Qualified surface-form evaluation over a specified length | Runout relative to an external datum unless evaluated separately | Sampling coverage, datum treatment where applicable and uncertainty |
| Circular runout (individual circular elements) | Datum-axis-referenced evaluation of the specified circular cross-sections, or a validated equivalent | Total runout of the full cylindrical surface or independent size conformity | Datum feature simulation, cross-section coverage, support and evaluation method |
| Total runout (entire specified surface) | Datum-axis-referenced evaluation across the controlled axial extent, or a validated equivalent | Separate diameter-size conformity without an appropriate size check | Datum feature simulation, lengthwise coverage, measurement strategy and uncertainty |
| Assembly fit or motion | Relevant functional gauge or mating-part test | Root cause of a failure or all independent GD&T requirements | Mating component, load, orientation and acceptance criterion |
Agree on Measurement Conditions and Final Acceptance Rules
Before approval, agree on the drawing callout, reference datums, measured length and locations, material state, part support, measurement method and acceptance rule. Probing density, filtering, fixture force or a different datum simulation can change the reported value. Close-to-limit results may also require an agreed treatment of measurement uncertainty.
The support condition during straightness verification can materially affect the reported result. Gravity sag, the distance between V-blocks, clamping force and the fitting method all matter for slender pins. Record support locations, part orientation, measured extent and the specified unloaded or functionally restrained condition where applicable, especially when the customer and supplier use different equipment.
First samples need detailed enough measurements to establish process feasibility and locate variation. Production inspection may then combine in-process checks, periodic form measurements and functional gauges as the control plan requires. Inspection frequency should reflect feature criticality and process evidence. Before approval, compare the customer and supplier setups for critical features so that the two methods measure the same characteristic.
Final inspection: The drawing callout, final process state, measurement method and acceptance rule must describe the same controlled feature and compatible reference condition. Where later heat treatment, coating or grinding can change that feature, an earlier passing result cannot serve as final acceptance.

Release condition: Inspect the finished part in the agreed condition, using the drawing’s datum references and the specified evaluation method.
For XTMIM’s general measurement resources, see inspection and testing. The ability to measure a particular roundness, straightness or runout limit must still be confirmed for that feature and inspection setup.
06 / Apply the complete decision chain
Worked Engineering Review: A Stepped MIM Pin with One Critical Journal
Representative Engineering Scenario · Illustrative only
The stepped pin described here is hypothetical. The process choices and acceptance criteria are conditional, not measured XTMIM production results.
Initial drawing: A small pin has an integrated head, shoulder, cross hole, general body and one short sliding journal. The preliminary drawing requests a tight diameter and ground finish along the entire outer length, although only the short journal guides sliding motion and the shoulder sets axial position. The rest of the body may not need the same finishing requirement.
Identify Functional Zones and Straightness Risks
The journal controls sliding fit and lateral guidance; the shoulder face establishes axial seating; the remaining body mainly provides clearance and structural connection. Specify the journal’s final diameter, relevant form and surface texture. The drawing must also control any required axial distance or face orientation between the journal and shoulder. If runout matters, reference the cylindrical datum feature(s) that establish the reference axis; a shoulder face alone cannot establish a rotation axis. Straightness should apply to the length that actually affects guidance or assembly.
The head, cross hole and change in section can affect sintering support and finishing access. Check the intended support orientation, handling state, journal-to-shoulder distance and feasible holding regions. Neither a fixed amount of bow nor the ability of grinding to correct it should be assumed without trial evidence.
Select the Finishing Route and Confirm the Inspection Plan
A proposed process route would mold the head, cross hole and shoulder near-net shape, then debind, sinter and complete any required material treatment. The sliding journal would be ground only if representative parts show that its as-sintered condition cannot meet the functional requirement and the proposed fixture has adequate access and stock. The body may remain as-sintered if its own clearance and geometry checks pass.
Before tooling approval, verify that the pin can be held for finishing without unacceptable bending and that the journal has sufficient stock around its full circumference. Inspect the shoulder’s axial location or face orientation wherever the drawing specifies them. If the journal has a runout requirement, inspect it relative to the designated cylindrical datum axis, not an axis inferred from the shoulder face. Each planned operation must be validated against the required final geometry.
Set a four-stage verification plan: (1) measure sintered and heat-treated straightness and pre-finish journal stock; (2) confirm that the fixture reproduces the drawing datum without distorting the part; (3) inspect the finished journal’s size, circular form, texture and any specified datum relationship; and (4) repeat critical measurements on representative parts to examine variation. The sampling plan and acceptance criteria should follow the drawing and the project’s risk, not a generic MIM capability estimate.
| Review stage | Provisional decision | What must be verified |
|---|---|---|
| Function | Classify one short sliding journal as critical; treat general body separately | Mating clearance, journal form / texture, shoulder axial seating and any specified datum axis |
| MIM geometry risk | Review head, cross hole, length and sintering support together | Actual straightness and repeatability after sintering / treatment |
| Manufacturing route | Evaluate near-net-shape body and selective journal grinding | Access, local stock, safe support, material condition and finish feasibility |
| Datum planning | Plan axial location from the shoulder face and any reference axis from designated cylindrical datum features | Axial/face relationship, datum simulation and finishing-to-inspection correlation |
| Final approval | Inspect the finished journal and specified assembly-critical relationships | Final-condition journal size/form, shoulder axial/face control and datum-based runout if called out |
Trial results determine the route. Whether the journal can remain as-sintered or needs finishing depends on its measured final condition, the available stock and the feasibility of controlling the required datum relationship. Different results call for different actions:
| Evidence from the drawing and trials | Engineering decision | Required confirmation before approval |
|---|---|---|
| The journal meets final-condition size, form, surface and applicable fit requirements as-sintered. | Keep the journal as-sintered. Do not add grinding solely because it is a shaft. | Repeatability across representative samples and a defined production control plan. |
| Only the local journal fails its required size, circular form or texture; usable stock and stable workholding are demonstrated. | Trial selective journal grinding. Retain the rest of the body as-sintered only where it passes its own requirements. | Finished journal measurements, stock cleanup, fixture repeatability and final material condition. |
| Journal diameter passes, but a specified runout relationship to a cylindrical datum axis fails. | Review datum transfer and finishing alignment before assuming further size reduction will solve it. | Measurement against the correct drawing datum and a verified corrective setup. |
| The controlled shaft length shows unacceptable bow or straightness variation. | Investigate upstream support, thermal distortion and validated correction; reconsider the route if stability cannot be achieved. | Final-state straightness over the specified length and consistent results across trials. |
| A geometrically simple pin requires precision finishing along nearly its full length. | Compare the complete MIM and turned-stock routes before committing to tooling. | Material, volume, tooling, machining, inspection, lead-time and quality-risk comparison. |
Tooling-release criterion: Release the chosen manufacturing route only when representative trials support final-condition size, form, datum relationships and an agreed production control plan. Where they do not, revise sintering support, finishing or fixture design, validate a suitable correction, or compare another manufacturing process. A passing intermediate measurement is not sufficient for release.
Record the decision: State the accepted route, which feature drove the choice, the drawings and inspection methods used, outstanding stock or fixture risks, and the responsible approver before tooling release. This record lets design, production and quality teams work from the same decision rather than a general instruction to grind the journal.
When MIM may not be the best route: A simple cylindrical pin with no integrated features and strict diameter and straightness requirements over almost its entire length may have little need for MIM. Compare the full MIM route with bar-stock turning or another process, including expected volume, material, finishing, inspection and quality risk.
Before Tooling: Final Drawing and RFQ Checklist
A 3D model alone cannot establish which surfaces need grinding or how the finished shaft will be accepted. Provide the drawing, assembly function and process information needed to make those decisions:
- Geometry: 3D STEP model, dimensioned 2D drawing, critical journal locations and controlled lengths.
- Function: mating-part dimensions, clearance/press-fit/slide/rotation/seal requirements and known assembly issues.
- GD&T: specified size, roundness, straightness, cylindricity/runout as needed, and applicable drawing standard.
- Datums: functional datum scheme and any suggested finishing or inspection datum conditions.
- Material state: material grade, heat treatment, target condition and special surface/texture requirements.
- Finishing: current or proposed grinding/turning/straightening operations, coatings and critical access restrictions.
- Demand: expected annual volume, batch size and existing production route if replacing an incumbent process.
- Acceptance: intended measurement method, first-sample evidence and production inspection expectations.
Unspecified functional journals can be over- or under-finished. Missing datum definitions can cause conflicting runout results. If the final heat-treatment condition is unclear, an earlier inspection may become irrelevant; without production volume, tooling and grinding economics cannot be compared reliably.
Frequently Asked Questions About MIM Shaft and Pin Grinding
Do all MIM shafts and pins require grinding?
No. Start with each surface’s function and the verified as-sintered condition. A clearance body may need no grinding; a critical journal may require local finishing. The correct choice follows the drawing, mating fit and process evidence rather than the component name.
Can circular runout pass while total runout fails?
Yes. Circular runout evaluates individual circular elements relative to the specified datum axis, whereas total runout evaluates the controlled surface over its full extent. Changes along the journal can therefore matter even when individual sectional checks pass. Apply the drawing’s actual callout and agreed inspection setup.
Can grinding a short journal straighten an entire bowed MIM pin?
Not automatically. Selective grinding establishes the finished surface relative to its setup; untreated shaft sections can retain bow or a mismatched axis. Measure the specified straightness length and investigate sintering support, treatment and fixture behavior before choosing a correction.
Should a MIM shaft journal be ground before or after heat treatment?
It depends on alloy, final hardness, thermal movement, finishing access and the required accepted condition. Verify the controlled geometry after the last operation that can change it. Neither sequence is universally correct for all MIM materials.
Is centerless grinding the default choice for all MIM pins?
No. It may suit certain continuous cylindrical features, but short journals, heads, shoulders, grooves or a specific datum relationship can require a different grinding setup or another finishing operation. Verify workholding, clean-up stock and the final inspection method.
What evidence should accompany a MIM shaft straightness or runout RFQ?
Provide a 3D STEP model and dimensioned 2D drawing showing controlled features and lengths, the governing GD&T system, datum references, mating fit, material/heat treatment, annual and batch quantities, expected final finish and the proposed measurement/acceptance method. Identify any observed assembly issue separately from a suspected cause.
Drawing Standards and Evidence Note
Use the GD&T or GPS system and edition specified on the customer drawing. ASME Y14.5 and ISO 1101 provide established approaches to geometrical requirements, but their default rules should not be mixed. The industry references below explain general MIM processing and inspection concepts; they do not establish a specific XTMIM process capability. Apply detailed clauses only after reviewing the relevant standard text.
Technical References
- ASME Y14.5 — Dimensioning and TolerancingOfficial GD&T standard overview; use the edition governing the drawing.
- ISO 1101:2017 — Geometrical TolerancingOfficial ISO overview of geometric specification and interpretation.
- MIMA — Complex Designs with MIMDesign considerations for sintering supports, long spans and thickness transitions.
- MPIF — Metal Injection Molding Process OverviewIndustry association background on molding, debinding and sintering.
- MIMA Case Study — Stainless Steel Shaft AssemblyIndependent industry example illustrating that an integrated MIM shaft route can still require straightening and finishing; not an XTMIM production case.
Submit a Shaft or Pin Drawing for Engineering Review
Send the 2D drawing and 3D model with critical cylindrical zones, mate/fit requirements, material condition, annual volume, required surface texture, datum scheme and final acceptance method.
The review should identify which surfaces can remain as-sintered, which journals may need grinding, how the sintering and heat-treatment route affects form, and how the final feature will be measured. Unresolved stock, datum or fixture constraints should be identified before tooling.







